Every factor, every assumption, every place we rounded against ourselves.
If a number appears anywhere on this website, its derivation is on this page. That is the whole point of having a methodology page rather than a sustainability slogan.
Quote: Impact Methodology
Component masses used throughout the site.
| Component | Mass | Source | Notes |
|---|---|---|---|
| Inner HDPE bottle | 42 lb / 19.1 kg | Weighed, n=140 | Mean across four moulders, ±3 lb |
| Steel cage | 55 lb / 24.9 kg | Weighed, n=140 | Galvanised, standard 275 configuration |
| Steel pallet | 31 lb / 14.1 kg | Weighed, n=96 | Composite base averages 36 lb total, plastic 28 lb |
| Valve, cap and gaskets | 2.4 lb / 1.1 kg | Weighed, n=60 | Excluded from avoided-impact figures |
| Total tare, steel base | 127 lb / 57.6 kg | Derived | Matches published manufacturer figures |
Carbon and water factors.
| Factor | Value used | Published range | Our choice |
|---|---|---|---|
| Virgin HDPE, cradle to gate | 1.86 kg CO₂e / lb | 1.8–2.4 | Low end |
| Virgin steel, cradle to gate | 0.86 kg CO₂e / lb | 0.8–1.3 | Low end |
| Wash cycle, per unit | 2.3 kg CO₂e | Measured | Includes heat recovery credit |
| Fresh water, per wash | 11.5 gal | Metered 2025 | Actual annual mean |
| Process water, virgin HDPE | 4.1 gal / lb | 3.8–11 | Low end |
| Process water, virgin steel | 1.2 gal / lb | 1.1–4 | Low end |
| Mature tree sequestration | 21.8 kg CO₂e / yr | 18–25 | Mid range |
| Truck CO₂e per mile | 0.40 kg / mile | 0.35–0.52 | Low end |
| HDPE recovery rate, our line | 68% | Measured | Actual, after label and residue loss |
| Steel recovery rate | 92% | Measured | Actual, mill-confirmed |
Where a published range exists, we use the low end for anything that makes our numbers look better and the high end for anything that makes them look worse. This systematically understates our impact, which is the direction we want to be wrong in.
What is inside and outside the system boundary.
Inside
- Avoided manufacturing emissions of containers not purchased new
- Our wash bay energy, water and chemistry
- Our reconditioning bench energy
- Material recovery yields measured at our own line
- Our own fleet fuel, for the transport figures only
Outside
- Your transport to and from our yard, because it depends on your geography
- Upstream carbon of new bottles bought for rebottling, beyond industry-average factors
- Downstream fate of HDPE flake after it leaves our building
- End-of-life of the valves, caps and gaskets, which are excluded from avoided-impact figures entirely
- Any form of offset, certificate or market instrument
Known limitations
Three, stated plainly. First, avoided-emissions accounting is inherently counterfactual: it depends on the assumption that a new container would otherwise have been bought, which is true for most of our customers and not all of them. Second, our scope 3 upstream data is industry-average rather than supplier-specific. Third, the mass factors are means with real variance across moulders, so a figure for a single unit carries more uncertainty than a figure for a fleet of two hundred.
Review
The factor table and the boundary definition get an external desk review each January by an independent consultant, who checks arithmetic and factor sourcing. That is a desk review, not a certified third-party verification, and we describe it that way deliberately.
The factors behind every number on this site.
| Factor | Value used | Published range | Our choice |
|---|---|---|---|
| Inner HDPE bottle mass | 42 lb / 19.1 kg | Weighed, n=140 | Measured mean |
| Steel cage mass | 55 lb / 24.9 kg | Weighed, n=140 | Measured mean |
| Steel pallet mass | 31 lb / 14.1 kg | Weighed, n=96 | Measured mean |
| Virgin HDPE, cradle to gate | 1.86 kg CO₂e / lb | 1.8 – 2.4 | Low end |
| Virgin steel, cradle to gate | 0.86 kg CO₂e / lb | 0.8 – 1.3 | Low end |
| Wash cycle, per unit | 2.3 kg CO₂e | Measured | Includes heat recovery credit |
| Fresh water per wash | 11.5 gal | Metered 2025 | Actual annual mean |
| Process water, virgin HDPE | 4.1 gal / lb | 3.8 – 11 | Low end |
| Process water, virgin steel | 1.2 gal / lb | 1.1 – 4 | Low end |
| Truck emissions | 0.40 kg CO₂e / mile | 0.35 – 0.52 | Low end |
| HDPE recovery, our line | 68% | Measured | After label and residue loss |
| Steel recovery | 92% | Measured | Mill confirmed |
Where a published range exists we use the end that makes our own numbers look worse. That systematically understates our impact, which is the direction we would rather be wrong in.
Where everything went in 2025.
| Disposition | Units | Share | Weight (lb) | Notes |
|---|---|---|---|---|
| Washed and resold as containers | 23,461 | 61.4% | 2,980,547 | Grades A, B and C |
| Reconditioned or rebottled | 7,222 | 18.9% | 917,194 | New bottles fitted: 4,118 |
| Upcycled into non-container products | 2,560 | 6.7% | 325,120 | 16 standard builds plus custom |
| Recycled to material | 2,751 | 7.2% | 349,377 | HDPE flake and baled steel |
| Energy recovery | 535 | 1.4% | 67,945 | Contaminated fractions only |
| Landfill | 1,681 | 4.4% | 61,428 | Gaskets, labels, adhesive, wash sludge |
Weights come from the yard scale, not from unit counts. We publish the landfill row rather than reporting only the diversion figure, because a diversion rate without a residual figure is a marketing number.
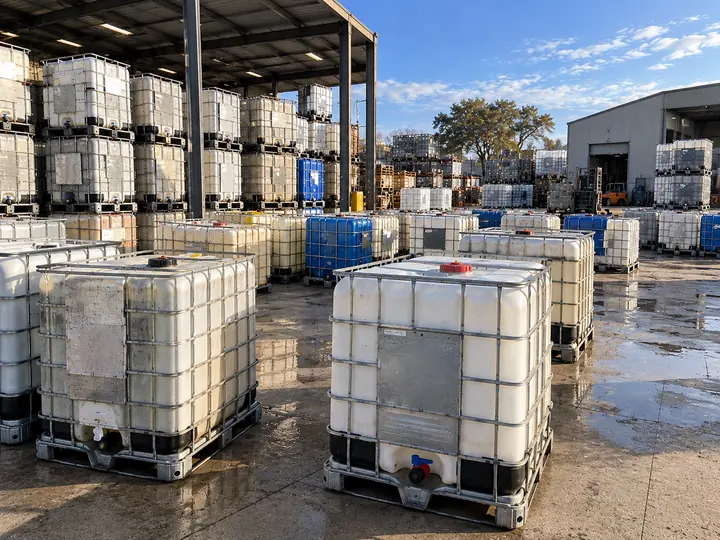
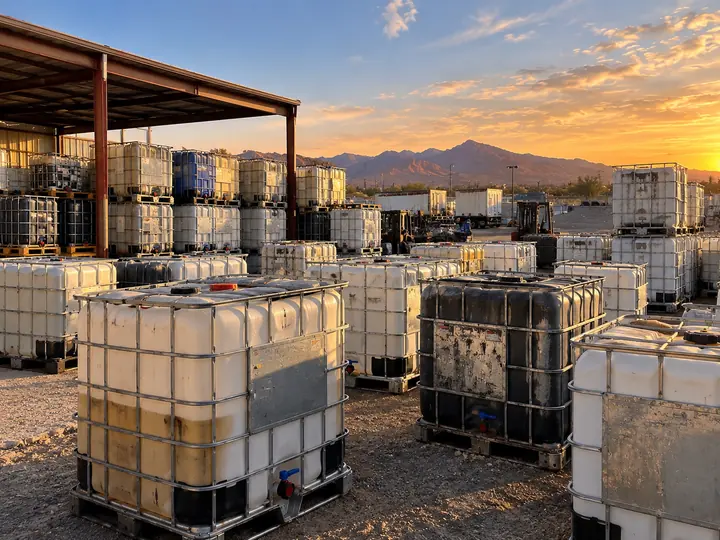
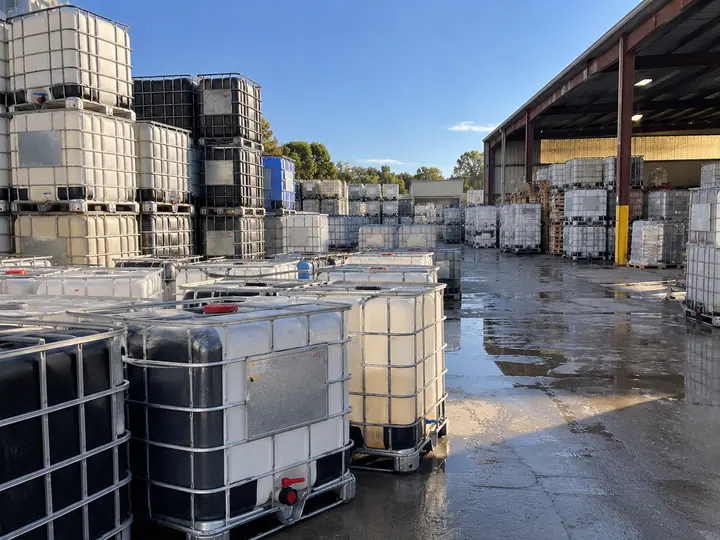
Three frames from the apron.
Grades side by side, plates facing out, and the load plan being executed. This is the whole business in three photographs.
The four wash routes and what each one logs.
| Route | Temperature | Chemistry | Rinses | Verification | Grade produced |
|---|---|---|---|---|---|
| 1 — Rinse only | Ambient to 100 °F | None or mild | 1–2 drained charges | Visual | B — rinsed |
| 2 — Hot caustic | 140–160 °F | Alkaline detergent, dosed | 3 cascade charges | Conductivity + scope | A — washed |
| 3 — Potable triple | 140–160 °F | Food-safe alkaline | 3 full potable charges | Conductivity vs supply + odour | A — food |
| 4 — Customer SOP | As specified | As specified | As specified | Every parameter logged | As agreed |
The route is chosen by prior cargo at the inspection stage, not by price at the sales desk. Fresh water use is 11.5 gallons per unit across all routes because the rinses cascade.
Ecology questions, answered at length.
Can I get a certificate for my sustainability report?
Yes, with every take-back collection: unit count, weighed mass, the split between resale, recondition, upcycle and recycle, and estimated CO₂e avoided referenced to the published factor table.
It is a much better figure than 'we recycle our containers', and it survives the question of where the number came from.
Is reusing a container actually better, or is washing it worse?
Better, by roughly thirty to one. A new 275-gallon composite IBC carries about 112 kg CO₂e of embodied impact. A wash cycle costs 2.3 kg CO₂e and 11.5 gallons of fresh water.
Reuse does not reduce embodied carbon; it amortises it. One cage across seven service lives divides the manufacturing impact by seven instead of paying it again each time.
Why do you publish your landfill figure?
Because a diversion rate without a residual figure is a marketing number. Anybody can say they divert 94% of their material.
Our 4.4% is mostly used gaskets, labels, adhesive residue and wash sludge. Gaskets are the largest contributor by count, they are thermoset, mixed and contaminated, and we genuinely cannot find anyone to take them.
Do you buy carbon offsets?
No, and we do not net anything against anything. Avoided emissions are reported as avoided emissions, separately from our own footprint.
Our trucks burn diesel — six tractors averaging 6.4 mpg. Milk runs and backhaul matching cut the miles per container by about 41%, which is real, but the fuel is still fuel.
Can my old bottles be recycled back into new tote bottles?
Realistically no, and anybody claiming otherwise is being loose with language. Post-industrial container flake carries prior-cargo risk and is not food-contact approved, and tote bottles are a demanding moulding application that wants consistent virgin-grade resin.
Our flake becomes drainage pipe, pallets and agricultural tubing at 68% recovery. Cages and pallets go to a regional electric arc furnace at 92% recovery.
Are your figures third-party verified?
No. The factor table and boundary definition get an external desk review each January by an independent consultant who checks arithmetic and factor sourcing.
That is a desk review, not certified verification, and we describe it that way deliberately. The full methodology, including three stated limitations, is published.
What arrives with the containers.
None of this is optional or chargeable. It is the difference between a reclaimed container and an anonymous second-hand one.
- A prior-contents sheet naming the product, the fill date and the company that filled it
- Four photographs of the actual unit plus an image of the cage stamp
- The grade assigned, and the published criteria that grade commits us to
- A wash record where the unit went through Route 2, 3 or 4, with temperature, dwell, rinse count and final rinse conductivity
- A leak test record for every Grade A and Grade B unit: method, pressure, hold time and measured decay
- The UN plate photograph and periodic test dates where the unit is marked
- A component list naming gasket material, valve type and cap type
- The cage passport ID, so the whole service history can be reissued later
- An allergen flag where a prior food cargo included dairy, egg or tree-nut oils
- A standing take-back offer: when you are finished, we collect and pay
How the operation actually runs.
Will you collect my empties?
Free from eight units inside our six weekly lanes, with payment for anything resaleable and a diversion certificate stating unit count, weighed mass and disposition split.
Further out, a collection needs to be close to a full trailer load or matched against a delivery on the same trip. We have never issued a disposal invoice.
How fast can you turn an order around?
Grade B and C from floor stock, usually the same week. Grade A washed, two to five business days. Rebottled, five to ten because bottles are fitted to order. Then add transit for your zone.
Wash bay throughput is about 90 units a day on Route 1 or 2 and 55 on Route 3. In practice turnaround is set by inspection and photography, not by washing.
Do you work with public buyers?
Regularly — municipalities, fire departments, school districts, county emergency management and state agencies.
Itemised quotes with freight on a separate line, W-9 and insurance certificates in one email, sealed bids where required, and we will hold stock against a purchase order that has not cleared yet if you tell us the situation.
Can you run a fleet programme for containers I own?
Yes, and it is a large part of what the bench does. Out full, back empty, washed, inspected, gasket replaced, leak tested, back on your fill line.
Priced per unit against a defined scope with a guaranteed turnaround, plus a quarterly fleet health report forecasting how many cages and bottles are approaching end of life. That report is the part customers say they value most.
What is the single best way to cut my container cost?
Measure your real cycle time, which is almost always worse than you think. Annual fills divided by fleet size: most operators assume eight turns a year and measure four to five.
Fleet size is throughput multiplied by cycle time, so halving cycle time halves the containers you need. Scheduled collection rather than requested collection is the single biggest lever, and it costs nothing.
Do you ship internationally?
Yes. Steel or plastic pallets to avoid ISPM 15 timber treatment requirements, double-stacked empties because ocean freight is priced per container, and a wash record plus prior-contents documentation in the pack.
Twenty-two units floor-loaded in a 40-foot container, forty-four double-stacked empty. Block and brace properly: ocean movement is far more violent in the vertical and roll axes than road movement.
The pages our own staff keep open.
When to retire a container, and what happens to it then.
| Trigger | Severity | Reusable parts | Material route | Take-back value |
|---|---|---|---|---|
| Crazing anywhere on the bottle | Absolute | Cage, base, hardware | HDPE flake, 68% recovery | Partial — cage and base credited |
| Wall loss over 15% of nominal | Absolute | Cage, base, hardware | HDPE flake | Partial |
| Failed leak test after repair | Absolute | Cage, base | HDPE flake | Partial |
| Heat or fire exposure | Absolute, no exceptions | Nothing — all refused | Energy recovery | None |
| Excluded prior cargo | Absolute | Nothing | Licensed disposal | None, and we will say why |
| Persistent bulge over 6 mm | High | Cage, base, hardware | HDPE flake | Partial |
| Cracked weld nodes, three or more | High | Bottle, base | Baled steel, 92% recovery | Partial — bottle credited |
| Base weld failure | High | Bottle, cage | Baled steel | Partial |
| Odour that will not clear | Medium | Cage, base, hardware | HDPE flake | Partial |
| Illegible UN plate | Medium — regulated service only | Everything | Stays in non-regulated service | Full |
| Cosmetic staining | None | Everything | Back to service as Grade C | Full |
| UV chalking, surface only | None for utility use | Everything | Outdoor service as Grade C | Full |
Our standing offer is the same for all of it: when you are finished with a container, we collect and pay, including for units we will only break for material. That is cheaper for us than buying the same steel and resin on the open market, which is the whole argument for a take-back programme existing at all.
Fourteen stations: what happens between the gate and the truck.
A container that arrives on a Monday morning and leaves as Grade A food on Thursday has been through fourteen stations, and at eight of them it can lose a grade or be pulled out entirely. This is the route, in order.
1 — Gate and declaration
Nothing comes off the trailer without a named prior cargo in writing. No name, no entry; the load goes back. This is the single rule that protects everything downstream, because one undeclared pesticide tote in a recirculating wash loop can affect a hundred units before anybody smells it.
2 — Exclusion screen
The declared cargo is checked against the published exclusion list. Pesticides, pharmaceutical actives, PFAS formulations, isocyanates, radiological material, fire-affected units and polymerising oils are refused outright, whatever the condition and whatever the price.
3 — Heel drain and measure
Residual cargo is drained, measured and routed to the correct waste stream. Under a gallon is normal. Above five gallons the load is a liquid-waste job rather than a container job, and it is priced or refused as one.
4 — Weigh and log
Yard scale, not a unit count. Every published tonnage on this site traces back to this scale, which is why our disposition table reports weight and units separately and why they do not divide into each other neatly.
5 — Cage and base inspection
Node by node, 44 to 54 of them, counted rather than sampled. Diagonals measured. Base welds loaded and watched. Galvanising checked at the welds, which is where it always goes first.
6 — Bottle condition
Wall thickness at four points, raking light across the whole surface for crazing, sump checked for stress whitening, mid-wall measured for bulge against a datum. This is where most grade losses happen, and none of them are about cleanliness.
7 — Wash route assignment
Decided here, by prior cargo, by an inspector — not at the sales desk by price. A food cargo goes to Route 3 whether the customer asked for it or not; an industrial cargo cannot buy its way onto Route 3.
8 — Wash
Route 1 rinse, Route 2 hot caustic, Route 3 potable triple rinse, or Route 4 to a customer's own written SOP. Temperature, dwell, rinse count and chemistry dosing are logged against the cage ID as it happens, not reconstructed afterwards.
9 — Rinse verification
Third-rinse conductivity against the day's measured supply water, final pH, 360-degree internal scope, and an independent two-operator odour check with the cap off. Any one of them failing sends the unit back to station 8.
10 — Hardware
New gasket on every Grade A and B unit, no exceptions. Valve function-tested and replaced if scored. New cap. Adapter threads checked under a light. Tamper seal on anything food-grade.
11 — Leak test
Pneumatic pressure decay on the complete assembly, under 1 kPa loss in ten minutes. Method, pressure, hold time and measured decay are written to the record — a pass with no numbers behind it is not a leak test.
12 — Grade and passport
The grade is assigned against the published criteria and written to the passport with the cage ID, the wash route, the test dates and the operator who did it. Seven years of retention, reissuable on request.
13 — Photography
Four shots of the actual unit plus the cage stamp, bay number visible. These go to the customer before payment. It started as a way of ending arguments about Grade B and became our best quality control, because an inspector who knows the photograph goes out grades more conservatively.
14 — Bay and load plan
Into one of 168 numbered bays by grade and configuration, then load-planned against trailer capacity. Twenty on the floor, forty double-stacked empty. If your order is twenty-two units, this is the station where somebody emails you to suggest twenty or forty.
The sixteen standard builds, with real dimensions.
| Build | Donor | Finished size | Capacity | Lead time |
|---|---|---|---|---|
| Rain harvesting station, single | C, 275 gal | 40 × 48 × 50 in | 260 gal usable | 3–5 days |
| Rain harvesting station, linked pair | C, 275 gal ×2 | 40 × 96 × 50 in | 520 gal usable | 5–8 days |
| Raised planter, half-cut | D, 275 gal | 40 × 48 × 24 in | 14 cu ft of medium | 2–4 days |
| Raised planter, long trough | D, 330 gal | 40 × 48 × 18 in | 11 cu ft | 2–4 days |
| Compost tumbler, framed | C, 275 gal | 48 × 50 × 56 in | 260 gal | 5–8 days |
| Livestock water trough | B or C, 275 gal | 40 × 48 × 26 in | 120 gal | 2–4 days |
| Fire reserve tank, stencilled | C, 330 gal | 40 × 48 × 53 in | 330 gal | 4–6 days |
| Dust suppression skid | C, 275 gal | 40 × 48 × 46 in | 275 gal | 4–6 days |
| Fertigation mixing station | B, 275 gal | 40 × 48 × 58 in | 275 gal + pump | 1–2 weeks |
| Wash-down station with hose reel | B, 275 gal | 40 × 48 × 60 in | 275 gal | 1–2 weeks |
| Aquaponics sump | C, 275 gal | 40 × 48 × 30 in | 150 gal | 3–5 days |
| Ballast weight, filled and capped | D, 275 gal | 40 × 48 × 46 in | 2,294 lb filled | 1–2 days |
| Erosion barrier, linked run | D, any | Per site drawing | n/a | By drawing |
| Cage-only storage crate | Cage from D | 40 × 48 × 46 in | 35 cu ft | 1–2 days |
| Pallet-base work bench | Base from D | 40 × 48 × 34 in | n/a | 1–2 days |
| Custom fabrication | By specification | By drawing | By drawing | Quoted |
Every build uses stock that failed container service, which is the point: a bottle that cannot be trusted to hold a regulated cargo can hold rainwater for another fifteen years. Two fabricators run this bench, so capacity is finite — book ahead of spring.
Impact questions, answered with the arithmetic.
Does freight cancel out the benefit?
Not remotely, at the distances involved. At 0.40 kg CO₂e per mile for a trailer carrying twenty units, a 500-mile delivery is about 10 kg CO₂e per container. Avoiding one new tote is in the region of 150 kg CO₂e.
It matters at the margins, which is why we run six scheduled lanes and chase backhaul utilisation — 41% of our return legs are loaded. But no plausible freight distance in the lower 48 makes reuse the worse option.
What happens to the parts you cannot reuse?
HDPE goes to flake at 68% recovery after label and residue loss. Steel is baled and mill-confirmed at 92%. Contaminated fractions go to energy recovery — 535 units' worth in 2025, 1.4% of intake.
The genuine residual is gaskets, labels, adhesive and wash sludge: 4.4% of intake by unit count, 61,428 lb by weight. We publish it rather than rounding it away, and the weight comes from the scale rather than from a unit count.
How do you calculate avoided emissions?
Mass times factor, with every factor published. A reused container avoids the cradle-to-gate impact of the new one it displaced: 42 lb of HDPE at 1.86 kg CO₂e per lb, 55 lb of steel at 0.86, 31 lb of steel pallet at the same, less the 2.3 kg CO₂e of the wash cycle and the freight at 0.40 kg CO₂e per mile.
Where a published range exists we use the end that makes our own numbers look worse — 1.86 against a range up to 2.4 for HDPE, for example. That systematically understates our impact, which is the direction we would rather be wrong in.
Why do you publish a landfill figure?
Because a diversion rate without a residual figure is a marketing number. Ours was 94.2% diverted and 4.4% to landfill in 2025 — gaskets, labels, adhesive and wash sludge, 61,428 lb of it, weighed on the yard scale.
If a supplier quotes you a diversion percentage and cannot immediately tell you what the residual was and what it consisted of, the percentage is not measured. It is estimated, and estimates in this industry drift upward.
Is reuse really better than recycling?
By a wide margin, for this product. Recycling a tote recovers 68% of the HDPE and 92% of the steel and then spends energy turning flake back into a product. Reusing it spends 2.3 kg CO₂e on a wash and keeps 100% of both materials doing the job they were made for.
That is why our disposition table reads 61.4% resold as containers and 18.9% reconditioned, with recycling at 7.2%. Recycling is what we do when reuse has genuinely been exhausted, not as a first resort with a better story attached.
What is the water footprint of a wash?
11.5 gallons of fresh water per container, metered across 2025 and across all four routes, because the rinses cascade and 86% of bay water recirculates.
Against that, making the HDPE bottle it displaced would have used about 4.1 gallons per pound of process water on the low end of the published range — roughly 172 gallons for a 42 lb bottle — plus 1.2 gallons per pound for 86 lb of steel. The wash is not close to being the expensive part.
Can I use your numbers in my own reporting?
Yes, and the methodology document exists for that purpose: every factor, its published range, and which end we chose. Several customers put the disposition record for their own returned units into their annual reporting.
We will also tell you what we do not have: no third-party verified LCA, no certification scheme membership, and a solar installation that covers 31% of yard electricity rather than the number we hoped for, because phase two is sitting in a utility interconnection queue. That list is in the vendor pack too.
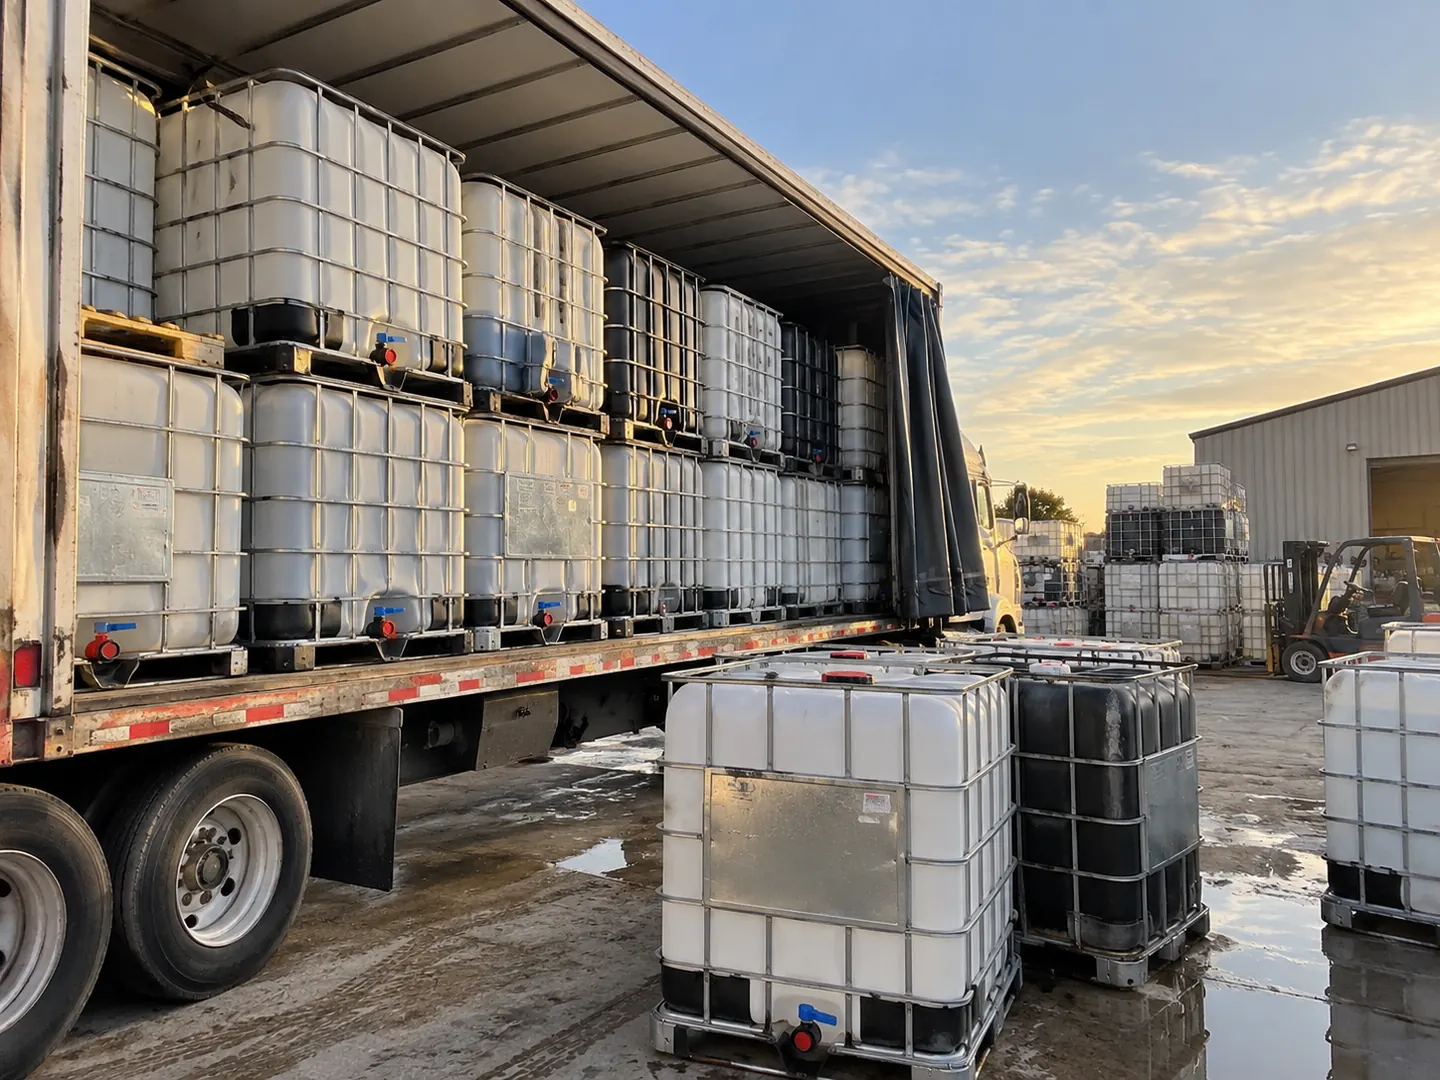
The yard at the hour we start.
Rinse verification: the numbers behind a wash record.
| Measurement | Method | Pass tolerance | What it actually proves |
|---|---|---|---|
| Third-rinse conductivity | Inline probe, µS/cm | Within 10% of supply water | No dissolved residue carrying over |
| Supply water baseline | Measured each shift | Logged, not assumed | The comparison has a real datum |
| pH of final rinse | Probe | 6.5 – 8.0 | Caustic or acid fully flushed |
| Visual, 360° internal scope | Borescope on a mast | No film, no shadow, no deposit | Nothing clinging above the heel line |
| Odour, cap off, ambient | Two operators independently | Neither detects cargo | The check a buyer will make themselves |
| Wash temperature | Bay thermocouple, logged | Route 2 and 3: 140–160 °F | The chemistry ran where it works |
| Dwell time | Cycle timer, logged | Per route specification | Not a quick splash through |
| Rinse count | Counted charges, logged | Route 3: three full potable | Dilution did the work, not optimism |
| Drain-down | Inverted dwell | Under 100 ml retained | No pooled water to go stale in storage |
| Leak test after wash | Pneumatic pressure decay | Under 1 kPa in 10 min | The wash did not find a weakness |
Conductivity against the day's supply water is the measurement that matters, and it is the one most wash records leave out. A number with no baseline is decoration. Ask any supplier what their third rinse read and what the tap read that morning.
Selling us your empties, in six steps.
We buy containers in any condition, including units that will fail every test. Material has value, and a collection that only takes the good ones leaves you with a disposal problem.
1 — Count and name the cargo
How many units, what size, and what was in them — product name and the company that filled them. The cargo decides the price and whether we can take them at all; the condition decides the rest.
2 — Photographs, rough is fine
A phone photograph of the stack and a couple of close-ups of the worst units. We are not grading from photographs, we are checking for the obvious disqualifiers before sending a truck.
3 — Written offer, per unit, by condition band
Not one number for the lot. Good units, utility units and reclaim units are priced separately, so you can see what you are being paid for rather than taking an average on trust.
4 — We schedule onto a lane
If you are on one of our six weekly routes, collection is usually inside the week and costs nothing. Further out we combine with a delivery going your way, which is what backhaul utilisation of 41% is for.
5 — Weighed and counted on arrival
Yard scale, against the manifest. Any discrepancy comes back to you with the scale ticket, in both directions — we have paid out more than was offered more than once.
6 — Payment, and a disposition record
Payment on agreed terms, plus a written record of where your units actually went: resold, rebottled, upcycled, recycled to material, or the residual fraction. Several customers use that record in their own reporting, which is why it exists in that format.
New container against reclaimed, without the sales pitch.
There are jobs where a new container is the right answer. We would rather say so than sell you the wrong thing and collect it back in a year.
Buy new when
- The cargo is a regulated Packing Group I material
- You need a specific design type, pressure rating or exotic liner nobody reclaims
- Your customer's audit requires virgin packaging in writing
- The product carries an allergen claim and rebottled will not satisfy the auditor
- You need five hundred identical units with identical plate dates on one date
- The container is part of a sealed, validated single-use process
Buy reclaimed when
- The cargo is water, glycol, fertiliser, a utility liquid or an unregulated industrial product
- A documented prior cargo and a published wash route satisfy your requirement
- You want the same container at 30 to 60 percent of the new price
- You want the impact figure, and the methodology behind it, in your own reporting
- You need units this week rather than on a moulder's lead time
- You want rebottled: a new HDPE bottle in an inspected cage, which is new where it touches the cargo
Rainwater harvesting with reclaimed totes, done properly.
This is the most common non-industrial use of a reclaimed tote and the one where the mistakes are most consistent. The design brief is simple: get roof water in, keep light and insects out, and let the overflow leave in a controlled direction.
Choose the right donor
Grade B or C, and black or painted rather than translucent. Light is the enemy: a translucent bottle in the open grows algae within one season and loses measurable wall thickness to UV within five. We paint or wrap every harvesting build for this reason. Never buy Grade A food stock for rainwater — you are paying three times the price for a wash route that the first leaf of autumn makes irrelevant.
Weight, which people underestimate
A full 275-gallon tote weighs about 2,420 lb. That is a small car on four square feet of footprint. It needs level, bearing ground — compacted gravel, pavers or a concrete pad — and it must not sit on soft soil that will subside on one corner and rack the cage. Never stack filled harvesting units. Never place one above anything you care about.
Inlet
Cut the 6-inch top port, fit a mesh basket strainer and a first-flush diverter. The diverter sends the first few gallons off the roof — the ones carrying the bird mess and the grit — away from the tank, and it is the difference between water you can irrigate with and a sump full of sludge. Keep the whole inlet path light-tight.
Overflow
The thing most builds get wrong. Every tank will overflow, and the only question is whether you chose where. Fit an overflow at least as large as the inlet, below the top of the tank, directed away from foundations. An unplanned overflow finds the top cap and runs down the cage into whatever the tank is standing on.
Outlet
The factory 2-inch valve with a camlock adapter and a GHT reducer handles a hose or a pump. Gravity gives you roughly 1.5 psi at the outlet for every three and a half feet of head, which is enough to fill a watering can and not enough for a sprinkler — so plan a pump if you want pressure.
Winter
Drain to below 85% before the first hard freeze, or empty entirely. Leave the valve open and the cap on. Ice in a full harvesting tote cracks the lower corner, and we see those units come back every March.
What the water is and is not
Roof runoff is non-potable. It is excellent for irrigation, washdown, dust suppression and toilet flushing where local rules allow, and it is not drinking water regardless of how clean the tank was. Keep it dark, keep it moving, and use it within a season rather than storing it over summer.
Washing, water and effluent.
What does a leak test actually involve?
Pneumatic pressure decay on the complete assembly: pressurise to the design test pressure, hold, and measure the loss. Our pass criterion is under 1 kPa in ten minutes, and the record states method, pressure, hold time and measured decay.
A leak test record with no numbers on it is not a leak test record. That is the single most useful thing to check on any supplier's paperwork, including ours.
Is there anything a wash cannot fix?
Plenty. Crazing, wall loss, a persistent bulge, cracked weld nodes, a failed base weld, heat exposure, an illegible plate — none of those are cleanliness problems and no wash route touches them.
And some cargo we will not try: pesticides, pharmaceutical actives, PFAS formulations, isocyanates, polymerising oils, radiological material, anything fire-affected, and anything nobody will name in writing. Those are refused at the gate, because the downside of being wrong is a drained loop and a contaminated batch.
What is the difference between rinsed and washed?
Route 1 is a rinse: one or two drained charges at ambient to 100 °F, verified visually. It produces Grade B and it is appropriate for a great deal of industrial and agricultural work.
Route 2 is a hot caustic wash: 140 to 160 °F, dosed alkaline detergent, three cascade charges, verified by conductivity and borescope. It produces Grade A washed. The gap between them is not a detail — it is the difference between a container that looks clean and one with a measured number behind it.
How can three rinses use only 11.5 gallons of fresh water?
Because the rinses cascade. The third rinse on one unit becomes the second rinse on the next and the first on the one after, so fresh water enters at the clean end and leaves at the dirty end. Eighty-six percent of bay water is recirculated.
It also means the direction of flow matters more than the volume, which is why the measurement we care about is third-rinse conductivity against the day's measured supply water rather than gallons used.
Can you get a cargo odour out completely?
Usually, and when we cannot the unit drops a grade and we say so rather than hoping you do not notice. Two operators check independently with the cap off at ambient temperature, because that is the check you will make yourself when it arrives.
The commonest cause of a lingering smell in an otherwise clean container is the gasket, not the bottle — the elastomer holds the prior cargo and no amount of rinsing the bottle addresses it. We fit a new gasket on every Grade A and B unit for exactly this reason.
What is ghosting, and does it matter?
A faint permanent shadow of a prior cargo visible through the bottle wall — most often from ferric chloride, a dye, or a strongly coloured fertiliser. It is cosmetic. The container holds and dispenses exactly as well as an unstained one.
It still costs a grade, because it means the prior cargo interacted with the polymer surface and because buyers reject it on sight. If you genuinely do not care how the tote looks, ghosted stock is some of the best value in the yard.
What happens to your wash water?
Eighty-six percent recirculates in the bay. The remainder goes to the sewer under an industrial wastewater discharge permit, whose number and latest sampling summary are in our vendor pack, and the sludge fraction is handled as a waste stream and appears in the residual line of our disposition table.
This is also why we will not advise you to pressure-wash a tote on your yard and let it run to a storm drain. That water is an effluent carrying your prior cargo, and in most jurisdictions it is a reportable discharge.
Rinsing a tote yourself: what works, what is theatre, and what is dangerous.
Sometimes you have a unit on site and a job to do. Here is what you can realistically achieve with a pressure washer and a hose, and where the line is.
First, the thing that is actually dangerous
Never put your head or an arm inside an IBC, and never let anyone else. It is a confined space. A tote that held a solvent, a fermenting product or anything that displaces oxygen can be lethal with no smell and no warning, and people die in containers this size every year. Everything below is done from outside the unit.
What you can do
A hot water rinse with a wand through the 6-inch port, three drained charges, will take a water-soluble cargo residue down to a level that is fine for irrigation, dust suppression, ballast or washdown. Drain fully between charges — dilution only works if the previous charge leaves. Invert or tip to drain the sump, because the heel is where everything concentrates.
What makes a real difference
Heat, agitation and a new gasket, in that order. Warm water does more than cold at any pressure. A spinning wand beats a static one. And replacing the gasket and cap costs a few dollars and removes the most common source of carried-over odour — the elastomer holds the prior cargo and no amount of rinsing the bottle addresses that.
What is theatre
One cold rinse and a sniff. Bleach into an unrinsed tote, which mostly produces a tote that smells of bleach and cargo. Detergent with no heat and no dwell time. And any process that does not include draining the sump, which is where the problem lives.
What you cannot do on site
Produce a food-grade container. Route 3 is three full potable charges at 140 to 160 °F with dosed food-safe chemistry, verified by third-rinse conductivity against measured supply water, a borescope and two independent odour checks. That is a bay, not a bucket. If the end use is food, potable water or anything with an audit behind it, buy rebottled or Grade A food — the premium is smaller than the risk.
And the legal bit
Your wash water is now an effluent carrying the prior cargo. Down a storm drain it is a reportable discharge in most jurisdictions. We hold an industrial wastewater discharge permit and publish the number in our vendor pack; a yard hose does not come with one.
How the container in your yard came to be shaped like that.
The modern caged IBC is a surprisingly young object, and almost every feature of it is the fossil of a specific problem.
Drums and nothing between
Liquids moved in 55-gallon drums or in bulk tankers. Anything in between meant handling dozens of drums, which is why the intermediate category was invented at all.
The first rigid composites
A blow-moulded plastic bottle inside a steel frame, sized to a pallet footprint so a forklift could handle it. The idea has not changed since.
The pallet footprint settles
40 × 48 inches in North America, 1,200 × 1,000 mm in Europe. Every trailer count on this site descends from that choice.
UN performance testing
Packagings began to be approved by design type and performance test rather than by prescription, which is where the 31HA1 marking family comes from.
Periodic testing arrives
The 2.5-year leak test and 5-year inspection cycle formalised, creating the date-stamped plate that decides whether a used unit can still carry a regulated cargo.
Reconditioning becomes a trade
Enough units in circulation, and enough value in a steel cage that outlasts three bottles, for washing and rebottling to be businesses rather than favours.
One bay and a used pressure washer
Re:IBCtote starts in a rented bay in metro Detroit, washing totes for local chemical blenders who could not get a straight answer about prior contents.
Grading gets published
We write down the disqualifiers rather than keeping them in an inspector's head, because the arguments about Grade B were taking more time than the washing.
The passport
Every unit gets a record keyed to its cage ID: intake, wash parameters, test results, grade, operator, dates. Seven-year retention, reissuable years later.
38,210 containers
Our largest year: 94.2% diverted, 4.4% residual published rather than rounded away, 4,281 tonnes of CO₂e avoided on factors we publish in full.
What the take-back programme pays.
Is it cheaper to buy twenty or to buy five, four times?
Twenty, nearly always, and the reason is freight rather than any volume discount on the containers. Twenty units fill the floor of a 53-foot van, so the freight per unit is at its lowest point on the whole curve.
The cliff is just past it: twenty-two units pays for two trailers to move two containers. If your number is anywhere near a trailer boundary, tell us it is flexible and we will tell you which way to move it.
Do you ever tell people to buy a cheaper grade?
Constantly, and it is the most reliable sales tactic we have. Roughly half the enquiries that ask for food-grade are for site water, dust suppression, ballast or fabrication, where Grade C does the same job for about a third of the price and lasts exactly as long under that treatment.
The money we lose on the first order we get back on the next four, and it means that when we do say you need rebottled, you can believe us.
What does take-back actually pay?
It depends on condition band and on what the cargo was, and we quote it per unit rather than as one number for the lot — good units, utility units and reclaim units priced separately so you can see what you are being paid for.
We pay for units that will fail every test, because a cage is 55 lb of steel at 92% recovery and a bottle is 42 lb of HDPE at 68%. Buying that material from you is cheaper for us than buying it on the open market, which is the whole economic argument for a take-back programme existing.
Why are containers and freight on separate lines?
Because a single delivered number hides which of a dozen variables you are paying for, and makes comparing two quotes impossible. Grade, wash route, hardware, pallet base, plate status, lane, season and quantity all move independently.
It also means that when you come back in six months, we can tell you whether the price moved because resin moved or because diesel moved. If a quote you are comparing does not split them, ask — the answer tells you something either way.
Is there a volume price, and at what point?
The real breaks are at trailer boundaries — twenty, forty, sixty — because that is where freight per unit steps down rather than drifting. Container pricing softens with volume too, but less than people expect, because the cost is dominated by wash bay time and bay time does not get cheaper in bulk.
Scheduled programmes are a different conversation: if you need forty units a month every month, we can hold stock and plan wash capacity around you, and that is worth more to both of us than a one-off discount.
When in the year should I buy?
Late summer for Grade B and C, if your timing is flexible. March to May is the agricultural pull and it puts fifteen to twenty percent on those grades while leaving Grade A almost untouched.
June to August is the softest point of the year on the grades that actually move seasonally. Buying Grade B in August rather than April is the single easiest saving available in this market, and it costs you nothing but storage space.
Do you charge for the documentation?
No, and we would rather you did not ask it as a question, because a supplier who charges for a wash record is telling you the record is a product rather than a byproduct of the process.
The prior-contents sheet, wash record, leak test, plate photograph, component list and passport ID come with every order. The vendor pack — W-9, insurance certificate, wash SOP, discharge permit, methodology, and the signed statement of what we are not certified for — arrives in one email, usually inside the hour.
The anatomy of a caged tote, part by part.
A 275-gallon caged IBC looks like one object and is actually five, each with a different lifespan, a different failure mode and a different second-hand value. Knowing which part you are buying is most of what separates a good purchase from an expensive one.
The inner bottle
Blow-moulded HDPE, 42 lb, nominal wall around 2 mm with deliberate thickening at the corners and the sump. It carries the cargo and nothing else. It is the part that ages: UV takes the surface, freeze-thaw cycling takes the corners, aromatic solvents soften the wall, and chemical stress plus mechanical stress together produce crazing. A bottle in indoor service with a compatible cargo will outlive the person who bought it. The same bottle in a Michigan yard, translucent, filled to the brim in November, has about five years.
The steel cage
Tubular galvanised steel, 55 lb, 44 to 54 welded nodes depending on the moulder. It takes every load the bottle cannot: stacking, strapping, forklift abuse, the hydrostatic push of a full bottle against its own walls. Cages outlast bottles roughly three to one, which is why rebottling exists as a trade at all. The failure modes are cracked nodes, a diagonal pushed out of square by impact, and red rust bleeding through a breached galvanising layer at a weld.
The base
Steel, composite, hybrid or timber, 22 to 44 lb. It decides how the unit can be handled and whether it can leave the country. Four-way entry and pallet-jack access are not universal, and a timber base without an ISPM 15 heat-treatment stamp will be stopped at a border. The welds attaching the cage to a steel base are a specific inspection point because a failed base weld makes the whole unit unstable under load with no other visible symptom.
The closures
A 6-inch top cap, a 2-inch discharge valve, the adapter stack at the outlet, and the gaskets. Together they weigh a few pounds, cost a fraction of the assembly, and cause most of the complaints: weeping valves, carried-over odour, cross-threaded adapters, vented caps left on in storage. We replace the valve, cap and gasket on every Grade A unit for exactly this reason — it is the cheapest possible insurance against the most common possible problem.
The markings
The UN plate, the cage stamp, the moulder's date wheel inside the bottle skirt. These are the unit's identity. The plate decides whether it can carry a regulated cargo and until when; the cage stamp is how we can reissue a seven-year service history years after the unit left the yard. A unit with an illegible plate is not scrap — it is a perfectly good container that has lost its licence, and it is priced accordingly.
If you only remember one thing: you are buying a bottle with a date on it, bolted into a cage that will outlive it, with hardware that should be new. Price the bottle, inspect the cage, insist on the hardware.
The same containers, different weather.
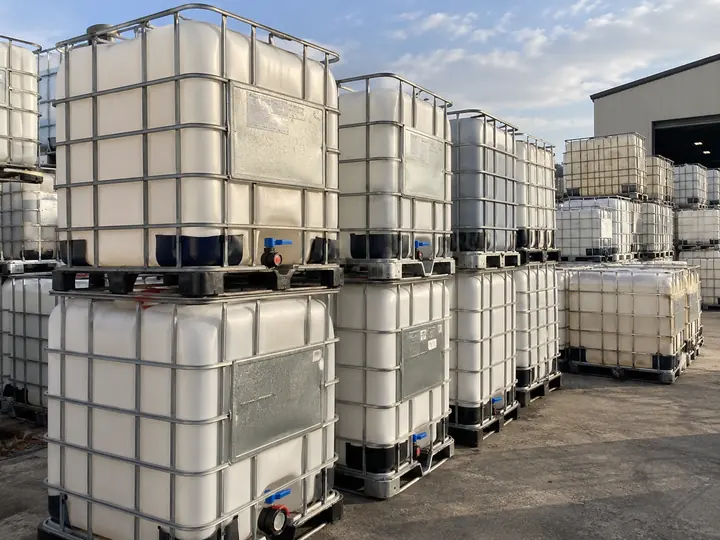
“An inspector who knows the photograph goes to the customer grades more conservatively. We started photographing every unit to end an argument, and it turned into the best quality control we have.”
Send us the cargo, not the grade.
Tell us what is going in the container and what you are doing with it, and we will name the grade, say what would disqualify a unit from it, and tell you if something cheaper does the job. That last part is why people come back.