Everything we know about totes, written down properly.
No listicles, no 500-word SEO filler. Long pieces about materials, grading, freight arithmetic, cleaning chemistry and the parts of this industry nobody writes about.
Ask about anything you read here
2 articles
- How to cut a tote without ruining it, from someone who has ruined manyA practical guide to cutting, trimming and finishing an IBC bottle for planters, cisterns and grow beds — including the four cuts you should never make.
- A complete rainwater harvesting build from two reclaimed totes550 gallons, first-flush diversion, overflow management, winterisation and the mistakes we made on the first six we built.
3 articles
- Buying totes for drinking water: the honest guideWe sell water storage and we will not sell you a used bottle for it. Here is the full reasoning, plus what to do instead and how to maintain it.
- “Food grade” are two words that mean nothing on their ownThree entirely different claims hide behind the same phrase. Here is how to work out which one a supplier is making.
- Reading the cage stamp: how to find out how old a tote really isSellers quote 'recent' and 'late model'. The cage tells you the truth, if you know which three places to look and which numbers to ignore.
2 articles
- The anatomy of an IBC cage: forty-eight welds, explainedWhich welds carry load, which ones only locate, and the four that we check first because they fail first.
- Sump design, and the two percent you can never pump outThe small sloped volume at the front of every tote is the most carefully engineered part of the container, and the source of most residue complaints.
2 articles
- Nobody wants our used gaskets, and it is ruining our diversion rate4.4% of what comes through our gate goes to landfill. Most of it is rubber rings the size of a dinner plate, and we cannot find anyone to take them.
- The carbon maths of rebottling, worked out in publicEverybody quotes a percentage. Almost nobody shows the arithmetic. Here is ours, line by line, including the parts that work against us.
3 articles
- The economics of a 300-tote fleet rotation, modelled properlyBuy, rent or rotate? A full model of a mid-sized chemical blender's container fleet across five years, with the replacement curve nobody plans for.
- Why used tote prices move, and how to buy against the cycleResin prices, agricultural seasons, freight rates and scrap steel. Four inputs that explain almost all of the variation in what a reclaimed tote costs.
- The true cost per gallon: totes, drums and bulk delivery comparedContainer price is the smallest number in the equation. Here is the full arithmetic, including the three costs almost nobody counts.
3 articles
- The freeze mistake that costs Michigan more bottles than anything elseWater expands about nine percent when it freezes. A tote filled to the brim in November is a split bottle in January, and we see dozens of them every spring.
- Winterising an outdoor tote installation in the Upper MidwestA dated checklist for zones 4 through 6, built from sixteen winters of watching what breaks and in what order.
- In cold storage, condensation is the enemy — not freezingEverybody plans for ice. Almost nobody plans for the half-litre of water that forms inside the headspace of a cold tote every time the temperature swings.
4 articles
- Why we do not have a phone numberIt is not a cost-saving measure and it is not because we dislike talking to people. It is because of what happens to a quote after the call ends.
- What we turn away at the gate, and why the list keeps growingSeven categories of cargo we will not accept, one rule that overrides all of them, and the uncomfortable economics of saying no to a full trailer.
- Why reconditioners refuse unlabelled totes, from the insideA short piece about the economics of uncertainty, and why 'I think it was just soap' is the most expensive sentence in this industry.
- Why we photograph every unit, and what to look for in the picturesFour photographs per tote, 38,000 times a year. A note on why we do it and how to read a supplier's photos critically.
3 articles
- Twenty-two totes is the worst number of totes to orderA 53-foot trailer holds twenty. Order twenty-two and you pay for two trailers. The arithmetic of freight is simple and almost nobody does it before ordering.
- Shipping totes internationally: ISPM 15, markings and the paperworkTimber pallets, phytosanitary stamps, container stuffing arithmetic and the two documentation failures that strand shipments at port.
- The 40 × 48 problem: pallet jacks, forklifts and why totes are the shape they areOne pallet dimension, chosen by a grocery trade association in the 1960s, determines the shape of almost every liquid container in North America.
3 articles
- What five years in the sun does to a toteUV degradation of HDPE, measured on units we have actually pulled from the field, and why black bottles are worth the premium outdoors.
- What a bulged bottle is telling youFour causes, three of which are reversible and one of which means the tote is finished. How to tell them apart in under a minute.
- Why HDPE bottles craze, and how to spot it before you payCrazing is the failure mode that sinks more reclaimed totes than cracks, impacts and UV combined — and it is almost invisible unless you know the trick.
2 articles
- Measuring your real container turnover, and why it is worse than you thinkMost fleets believe they turn containers eight times a year. Measured properly, the median is closer to four, and the gap is sitting in somebody's yard.
- How to inventory a yard full of totes in one afternoonYou have inherited two hundred containers and no records. A practical field method that gets you a usable asset register before it gets dark.
2 articles
- Agitators, mixers and keeping a slurry in suspensionSettling is the problem that turns a good cargo into two bad ones. What actually works in a 275-gallon rectangular vessel, and what does not.
- A field guide to IBC valves, and why yours is leakingButterfly, ball, diaphragm and the dreaded moulded-in plug. Five leak paths, in the order you should check them.
4 articles
- Totes and fire codes: the six questions your inspector will askQuantity limits, containment, separation distance, sprinkler design and the plastic-container problem. A plain-language orientation, not legal advice.
- Specific gravity: the number that breaks forkliftsA tote of water is 2,420 pounds. The same tote of 50% caustic is 3,510. Most warehouse forklifts are rated for the first number and not the second.
- Four stacking rules every warehouse breaks at least onceStack ratings are not advisory, they are not per-tote, and they do not survive a straightened cage. A short, blunt piece about the most dangerous thing in a tote yard.
- Static electricity and flammable liquids in plastic totesPolyethylene is an excellent insulator, which is exactly the problem. Why standard composite IBCs are the wrong container for Class I flammables, and what to use instead.
The grading system, in one table.
| Grade | Prior cargo | Wash route | Clean index | Price index | Drops a grade if |
|---|---|---|---|---|---|
| A — Food | One, food only, documented | Route 3 potable triple rinse | 100 | 100 | More than one cargo, missing declaration, film on scope, odour fail |
| A — Rebottled | None — new bottle | New, unused | 98 | 86 | Cage fails node inspection or leak test |
| A — Washed | Non-hazardous industrial | Route 2 hot caustic | 92 | 74 | Ghosting remains, or cargo history unverifiable |
| B — Rinsed | Mixed industrial | Route 1 rinse | 72 | 52 | Structural repair, or odour a buyer would notice |
| C — Non-potable | Heavier residue, repaired | Route 1 rinse | 48 | 34 | Any crazing, any persistent bulge, failed leak test |
| D — Reclaim | Failed test or structure | Not resold | 16 | 9 | Not applicable — this is the floor |
Price index is relative to Grade A food at 100, not a quote. The absolute level moves with resin, scrap steel, freight rates and the agricultural season.
Baseline specifications for everything we handle.
| Container | Capacity | Footprint | Height | Tare | Gross at SG 1.0 | Per 53' trailer |
|---|---|---|---|---|---|---|
| Caged composite IBC | 275 gal / 1,040 L | 40 × 48 in | 46 in | 127 lb | 2,420 lb | 20 floor / 40 stacked |
| Caged composite IBC, XL | 275 gal / 1,040 L | 40 × 48 in | 53 in | 132 lb | 2,425 lb | 20 / 40 |
| Caged composite IBC | 330 gal / 1,250 L | 40 × 48 in | 53 in | 145 lb | 2,900 lb | 20 / 40 |
| Caged composite IBC | 350 gal / 1,325 L | 48 × 48 in | 52 in | 170 lb | 3,090 lb | 18 / 36 |
| Stainless bin, 304 | 350 gal / 1,325 L | 48 × 42 in | 55 in | 420 lb | 3,340 lb | 18 / — |
| Stainless bin, 316L | 500 gal / 1,893 L | 52 in dia. | 74 in | 580 lb | 4,750 lb | 14 / — |
| Poly drum, closed head | 55 gal / 208 L | 23 in dia. | 34.5 in | 22 lb | 480 lb | 80 on pallets |
| Steel drum, lined | 55 gal / 208 L | 22.5 in dia. | 33.5 in | 38 lb | 496 lb | 80 on pallets |
| Salvage overpack | 95 gal / 360 L | 28 in dia. | 40 in | 35 lb | 827 lb | 40 on pallets |
Figures are nominal and vary a little by moulder. Always multiply net volume by the actual specific gravity of your cargo before checking a forklift or racking rating.
Three frames from the apron.
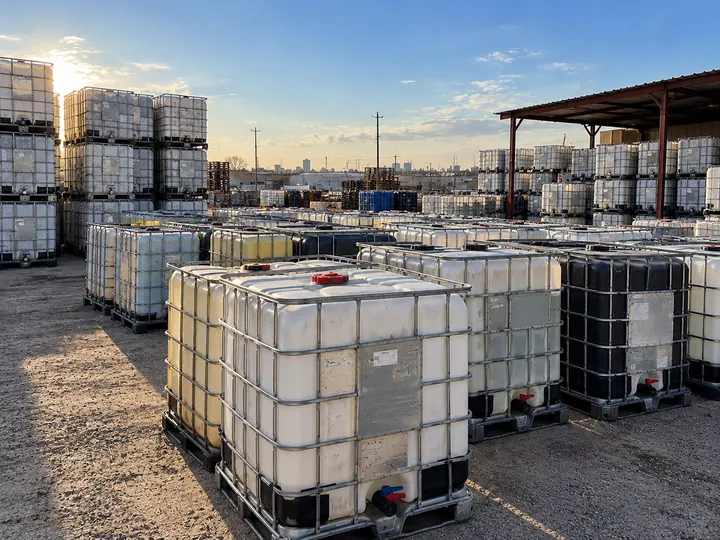
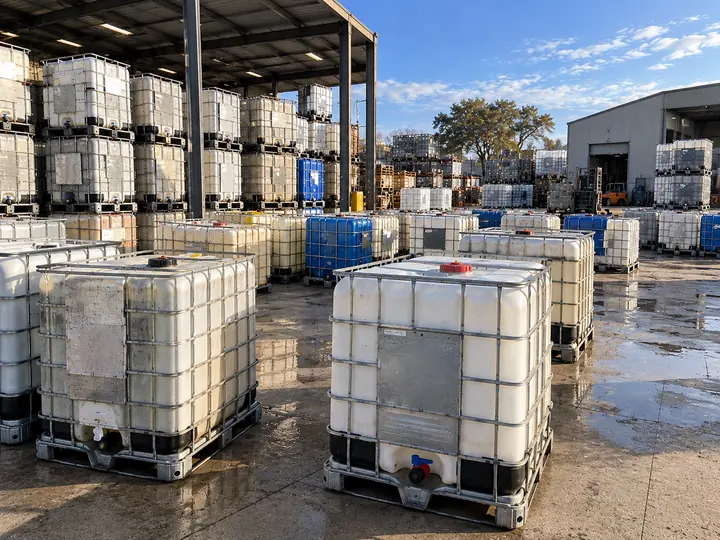
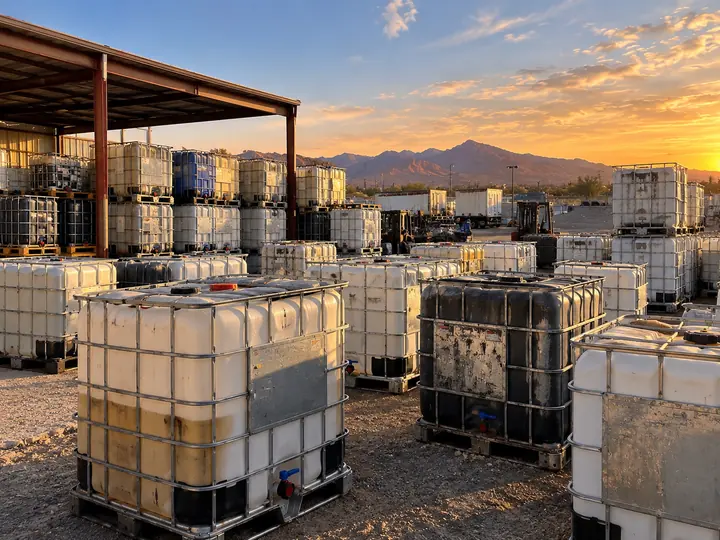
Grades side by side, plates facing out, and the load plan being executed. This is the whole business in three photographs.
What arrives with the containers.
None of this is optional or chargeable. It is the difference between a reclaimed container and an anonymous second-hand one.
- A prior-contents sheet naming the product, the fill date and the company that filled it
- Four photographs of the actual unit plus an image of the cage stamp
- The grade assigned, and the published criteria that grade commits us to
- A wash record where the unit went through Route 2, 3 or 4, with temperature, dwell, rinse count and final rinse conductivity
- A leak test record for every Grade A and Grade B unit: method, pressure, hold time and measured decay
- The UN plate photograph and periodic test dates where the unit is marked
- A component list naming gasket material, valve type and cap type
- The cage passport ID, so the whole service history can be reissued later
- An allergen flag where a prior food cargo included dairy, egg or tree-nut oils
- A standing take-back offer: when you are finished, we collect and pay
The pages our own staff keep open.
The anatomy of a caged tote, part by part.
A 275-gallon caged IBC looks like one object and is actually five, each with a different lifespan, a different failure mode and a different second-hand value. Knowing which part you are buying is most of what separates a good purchase from an expensive one.
The inner bottle
Blow-moulded HDPE, 42 lb, nominal wall around 2 mm with deliberate thickening at the corners and the sump. It carries the cargo and nothing else. It is the part that ages: UV takes the surface, freeze-thaw cycling takes the corners, aromatic solvents soften the wall, and chemical stress plus mechanical stress together produce crazing. A bottle in indoor service with a compatible cargo will outlive the person who bought it. The same bottle in a Michigan yard, translucent, filled to the brim in November, has about five years.
The steel cage
Tubular galvanised steel, 55 lb, 44 to 54 welded nodes depending on the moulder. It takes every load the bottle cannot: stacking, strapping, forklift abuse, the hydrostatic push of a full bottle against its own walls. Cages outlast bottles roughly three to one, which is why rebottling exists as a trade at all. The failure modes are cracked nodes, a diagonal pushed out of square by impact, and red rust bleeding through a breached galvanising layer at a weld.
The base
Steel, composite, hybrid or timber, 22 to 44 lb. It decides how the unit can be handled and whether it can leave the country. Four-way entry and pallet-jack access are not universal, and a timber base without an ISPM 15 heat-treatment stamp will be stopped at a border. The welds attaching the cage to a steel base are a specific inspection point because a failed base weld makes the whole unit unstable under load with no other visible symptom.
The closures
A 6-inch top cap, a 2-inch discharge valve, the adapter stack at the outlet, and the gaskets. Together they weigh a few pounds, cost a fraction of the assembly, and cause most of the complaints: weeping valves, carried-over odour, cross-threaded adapters, vented caps left on in storage. We replace the valve, cap and gasket on every Grade A unit for exactly this reason — it is the cheapest possible insurance against the most common possible problem.
The markings
The UN plate, the cage stamp, the moulder's date wheel inside the bottle skirt. These are the unit's identity. The plate decides whether it can carry a regulated cargo and until when; the cage stamp is how we can reissue a seven-year service history years after the unit left the yard. A unit with an illegible plate is not scrap — it is a perfectly good container that has lost its licence, and it is priced accordingly.
If you only remember one thing: you are buying a bottle with a date on it, bolted into a cage that will outlive it, with hardware that should be new. Price the bottle, inspect the cage, insist on the hardware.
Chemical compatibility, container by gasket.
| Cargo | HDPE bottle | EPDM | Viton | PTFE | Note |
|---|---|---|---|---|---|
| Water, potable | Excellent | Excellent | Excellent | Excellent | Rebottled or Grade A food only |
| Sodium hypochlorite 12.5% | Good | Fair | Good | Excellent | Vent — the cargo off-gasses and will bulge a sealed bottle |
| Caustic soda 50% | Excellent | Excellent | Good | Excellent | SG 1.53 — 275 gal only, check the forklift plate |
| Sulphuric acid 93% | Not suitable | Not suitable | Fair | Excellent | Lined steel or stainless service, never poly |
| Hydrochloric acid 35% | Good | Not suitable | Excellent | Excellent | Viton only; HCl destroys EPDM in weeks |
| Nitric acid 10% | Fair | Not suitable | Good | Excellent | Oxidiser — embrittles HDPE over months |
| Phosphoric acid 75% | Good | Fair | Good | Excellent | Common fertiliser intermediate |
| Propylene glycol | Excellent | Excellent | Excellent | Excellent | The most-handled tote cargo in the Midwest |
| Ethylene glycol | Excellent | Excellent | Excellent | Excellent | Label clearly — it is routinely confused with PG |
| Ethanol, 190 proof | Good | Fair | Excellent | Excellent | Flammable — conductive container and bonding required |
| Methanol | Good | Fair | Excellent | Excellent | Permeates slowly through HDPE; not for long storage |
| Mineral oil, white | Excellent | Not suitable | Excellent | Excellent | EPDM swells in hydrocarbons |
| Used motor oil | Excellent | Not suitable | Excellent | Excellent | Warm to 60 °F before pumping in winter |
| Diesel and heating oil | Good | Not suitable | Excellent | Excellent | Check local rules before storing fuel in an IBC |
| Vegetable and canola oil | Excellent | Good | Excellent | Excellent | Hot wash route afterwards or it polymerises |
| Urea solution 32.5% (DEF) | Excellent | Excellent | Excellent | Excellent | Freezes at 12 °F, expands, then recovers |
| Liquid fertiliser 28-0-0 | Excellent | Excellent | Excellent | Excellent | Stains the bottle; does not harm it |
| Ferric chloride 40% | Excellent | Not suitable | Excellent | Excellent | Permanent orange staining — cosmetic only |
| Hydrogen peroxide 35% | Fair | Not suitable | Good | Excellent | Vented cap mandatory; dedicated bottle, never reused |
| Acetic acid 80% | Good | Fair | Good | Excellent | Odour carries over — dedicate the unit |
| Latex paint and coatings | Excellent | Good | Excellent | Excellent | Never let it dry inside; a cured film is unremovable |
| Toluene, xylene, MEK | Not suitable | Not suitable | Good | Excellent | Aromatic solvents swell and soften HDPE |
| Isocyanates and polyols | Refused | Refused | Refused | Refused | On our published exclusion list — they cure |
| Firefighting foam concentrate | Refused | Refused | Refused | Refused | PFAS risk; we will not take it at any price |
Ratings are for ambient-temperature storage in a reclaimed container, not for pressurised or heated service. Every 20 °F above 100 °F roughly halves the service life of the rating. When the cargo is not on this list, send us the SDS and we will tell you what we would and would not put it in.
Fourteen stations: what happens between the gate and the truck.
A container that arrives on a Monday morning and leaves as Grade A food on Thursday has been through fourteen stations, and at eight of them it can lose a grade or be pulled out entirely. This is the route, in order.
1 — Gate and declaration
Nothing comes off the trailer without a named prior cargo in writing. No name, no entry; the load goes back. This is the single rule that protects everything downstream, because one undeclared pesticide tote in a recirculating wash loop can affect a hundred units before anybody smells it.
2 — Exclusion screen
The declared cargo is checked against the published exclusion list. Pesticides, pharmaceutical actives, PFAS formulations, isocyanates, radiological material, fire-affected units and polymerising oils are refused outright, whatever the condition and whatever the price.
3 — Heel drain and measure
Residual cargo is drained, measured and routed to the correct waste stream. Under a gallon is normal. Above five gallons the load is a liquid-waste job rather than a container job, and it is priced or refused as one.
4 — Weigh and log
Yard scale, not a unit count. Every published tonnage on this site traces back to this scale, which is why our disposition table reports weight and units separately and why they do not divide into each other neatly.
5 — Cage and base inspection
Node by node, 44 to 54 of them, counted rather than sampled. Diagonals measured. Base welds loaded and watched. Galvanising checked at the welds, which is where it always goes first.
6 — Bottle condition
Wall thickness at four points, raking light across the whole surface for crazing, sump checked for stress whitening, mid-wall measured for bulge against a datum. This is where most grade losses happen, and none of them are about cleanliness.
7 — Wash route assignment
Decided here, by prior cargo, by an inspector — not at the sales desk by price. A food cargo goes to Route 3 whether the customer asked for it or not; an industrial cargo cannot buy its way onto Route 3.
8 — Wash
Route 1 rinse, Route 2 hot caustic, Route 3 potable triple rinse, or Route 4 to a customer's own written SOP. Temperature, dwell, rinse count and chemistry dosing are logged against the cage ID as it happens, not reconstructed afterwards.
9 — Rinse verification
Third-rinse conductivity against the day's measured supply water, final pH, 360-degree internal scope, and an independent two-operator odour check with the cap off. Any one of them failing sends the unit back to station 8.
10 — Hardware
New gasket on every Grade A and B unit, no exceptions. Valve function-tested and replaced if scored. New cap. Adapter threads checked under a light. Tamper seal on anything food-grade.
11 — Leak test
Pneumatic pressure decay on the complete assembly, under 1 kPa loss in ten minutes. Method, pressure, hold time and measured decay are written to the record — a pass with no numbers behind it is not a leak test.
12 — Grade and passport
The grade is assigned against the published criteria and written to the passport with the cage ID, the wash route, the test dates and the operator who did it. Seven years of retention, reissuable on request.
13 — Photography
Four shots of the actual unit plus the cage stamp, bay number visible. These go to the customer before payment. It started as a way of ending arguments about Grade B and became our best quality control, because an inspector who knows the photograph goes out grades more conservatively.
14 — Bay and load plan
Into one of 168 numbered bays by grade and configuration, then load-planned against trailer capacity. Twenty on the floor, forty double-stacked empty. If your order is twenty-two units, this is the station where somebody emails you to suggest twenty or forty.
Reference answers on specification.
What does the stacking figure on the plate actually mean?
It is the permissible superimposed load: how much mass may sit on top of that container. It assumes normal temperature, level ground and an evenly distributed load, and a zero means do not stack even empty.
The real-world caveat is temperature. Above 100 °F derate by half; above 120 °F do not stack at all. HDPE creeps under sustained load and heat accelerates it, so a stack that was fine in April can deform in July without anything else changing.
How long does an HDPE bottle actually last?
Indoors with a compatible cargo, longer than the business using it — we regularly handle bottles over twenty years old that pass every test. Outdoors, translucent, filled to the brim through Michigan winters: about five years.
What kills them is the combination of UV, freeze-thaw cycling and chemical stress acting together. Any one is survivable. All three together produce crazing, and crazing is the one condition with no path back.
Is stress whitening the same as crazing?
No, and the distinction is worth money. Stress whitening is localised opacity where the polymer has been strained, almost always a forklift impact near the sump. It looks alarming and is often not a failure.
Crazing is a network of fine branching cracks from chemical and mechanical stress together. It is an absolute disqualifier, it never improves, and the test is a raking light at a shallow angle across the surface. If you can see branching, the bottle is finished — though the cage and base are still worth money.
Can a cage be reused with a new bottle?
Yes, and that is what rebottling is: a new blow-moulded HDPE bottle fitted into an inspected cage and base. Cages outlast bottles about three to one, which is why the trade exists.
The cage goes through the same inspection as everything else first — 44 to 54 weld nodes counted individually, diagonals measured, base welds loaded, galvanising checked at the welds. We fitted 4,118 new bottles in 2025. Bench turnaround on contract work is 48 hours.
Do you have 350 and 500 gallon containers?
Yes, as stainless bins rather than caged composites. A 350-gallon square 304 bin is 48 × 42 inches and 55 inches tall with a 420 lb tare; a 500-gallon cylindrical 316L is 52 inches in diameter, 74 tall, 580 lb.
They are the right answer for aggressive acids above SG 1.6, for hot cargo, and for anything where you want a container that will outlive several poly ones. They do not stack, and the trailer count drops to fourteen for the 500s.
What is the heaviest cargo you would put in a reclaimed poly tote?
In practice, 50% caustic soda at SG 1.53 in a 275 — which grosses 3,637 lb — is about where we stop being comfortable, and we check the customer's forklift rating before quoting it.
Sulphuric acid at 93% and SG 1.83 we will not put in poly at all; that is steel or stainless service. The limiting factor is rarely the bottle's burst strength and almost always everything underneath it: forks, beams, floors.
How do I work out whether my cargo is too heavy for a 330?
Multiply litres by specific gravity to get kilograms, or gallons by 8.34 by specific gravity to get pounds, then add the tare — 127 lb for a 275, 145 lb for a 330 — and compare against the maximum gross mass on the UN plate.
The plate figure is the binding one. As a rough guide, cargo above about SG 1.4 belongs in a 275 rather than a 330 simply because the taller bottle puts more mass on the same footprint, and above SG 1.6 you are usually looking at lined steel or stainless rather than poly.
The yard at the hour we start.
New container against reclaimed, without the sales pitch.
There are jobs where a new container is the right answer. We would rather say so than sell you the wrong thing and collect it back in a year.
Buy new when
- The cargo is a regulated Packing Group I material
- You need a specific design type, pressure rating or exotic liner nobody reclaims
- Your customer's audit requires virgin packaging in writing
- The product carries an allergen claim and rebottled will not satisfy the auditor
- You need five hundred identical units with identical plate dates on one date
- The container is part of a sealed, validated single-use process
Buy reclaimed when
- The cargo is water, glycol, fertiliser, a utility liquid or an unregulated industrial product
- A documented prior cargo and a published wash route satisfy your requirement
- You want the same container at 30 to 60 percent of the new price
- You want the impact figure, and the methodology behind it, in your own reporting
- You need units this week rather than on a moulder's lead time
- You want rebottled: a new HDPE bottle in an inspected cage, which is new where it touches the cargo
Symptom, cause, what to do about it.
| Symptom | Most likely cause | Check first | Fix |
|---|---|---|---|
| Weeping at the valve when closed | Seat compression set from long open storage | Close fully, wipe dry, watch 10 min | Replace the valve; store closed in future |
| Drip from under the valve body | Flange gasket, not the valve | Feel behind the valve for wet | Pull the valve, new flange gasket |
| Cargo odour in a clean tote | Original gasket retained, or cap gasket | Smell the gasket itself, off the unit | New gasket; re-rinse; air with the cap off |
| Bottle bulging at mid-wall | Overfill, heat, or off-gassing cargo | Cargo SDS for gas generation; ambient temp | Vented cap at point of use; reduce fill to 85% |
| Condensate on top of the cargo | Vented cap left on in storage | Which cap is fitted | Solid cap for storage; vent only when dispensing |
| Crack at the lower corner | Water-based cargo froze at full fill | Fill level history | Unit is finished — we will take it back for reclaim |
| White cloudy patch at the sump | Stress whitening from forklift impact | Raking light for branching cracks | Monitor; no crazing means serviceable, Grade C |
| Fine branching cracks | Crazing, from chemical stress or UV | Any raking light at a shallow angle | Retire the bottle; the cage and base are reusable |
| Flow stops mid-discharge | Vacuum lock — no air in | Crack the top cap and listen | Vent while dispensing, always |
| Slow flow on a cold morning | Cargo viscosity, not a blockage | Cargo temperature against its SDS | Warm the product; never heat the bottle directly |
| Adapter binds after two turns | Wrong buttress standard | Compare S60×6 / S70×6 / S75×6 | Correct adapter or a proper reducer; never force |
| Cage node cracked | Impact, or a stacked load over rating | Count cracked nodes; check plate stack rating | Do not stack; return for cage swap |
| Tote rocks on the forks | Base weld failed at one corner | Lift 2 in and look at all four welds | Take out of service immediately — transplant job |
| Rust bleeding through the zinc | Galvanising breached, usually at a weld | Wire-brush a test patch | Cosmetic for utility use; fails food-grade intake |
| Label illegible after a season | Direct-print on HDPE in UV | Whether the UN plate is also fading | Stencil and clear-coat, or stainless tag |
Temperature limits and the derating nobody mentions.
| Temperature | HDPE bottle | Steel cage | Gasket | Stacking allowed | Practical effect |
|---|---|---|---|---|---|
| Below −20 °F | Brittle | Fine | Hardened | No | Impact cracking at the sump corner; do not forklift a cold full tote hard |
| −20 to 32 °F | Serviceable | Fine | Stiff | Yes, derate 25% | Water-based cargo freezing; fill to 85% only |
| 32 to 100 °F | Full rating | Full rating | Full rating | Yes, full | Normal service window — every published figure assumes this |
| 100 to 120 °F | Softening | Fine | Fine | Derate 50% | Visible bulge in a full tote standing in July sun |
| 120 to 140 °F | Marginal | Fine | Check cargo | No | Creep accelerates; never stack, never rack |
| 140 to 160 °F | Short excursion only | Fine | EPDM limit | No | Wash bay territory — empty units only |
| Above 160 °F | Not suitable | Fine | PTFE only | No | Permanent deformation; the unit leaves as Grade D |
Heat-affected HDPE does not recover its original wall strength when it cools. This is why anything that has been near a fire is refused at our gate regardless of how it looks.
Reference answers on use.
How do I get the last of the cargo out?
Tip the unit forward slightly so the sump is the low point, and vent the top cap while you drain — most 'the valve is blocked' calls are a vacuum lock, not a blockage. Crack the cap and listen for air.
Expect to leave under a gallon as heel in a standard sump. If recovering that last gallon matters to your economics, ask about units with a dedicated discharge geometry rather than fighting a standard sump.
Can I cut a tote up myself?
People do, for planters and troughs, and it is straightforward with a jigsaw in the plastic and an angle grinder on the cage. Two warnings, both serious.
First, know what was in it: cutting into a bottle that held a solvent is an ignition risk, and never put your head or arm inside an intact container, which is a confined space that has killed people. Second, cut edges on HDPE are sharp and the cage tubes spring when relieved. Our fabricators build sixteen standard designs from Grade C and D stock, finished and deburred, if you would rather not.
What can I do with a tote that failed?
A bottle that cannot be trusted with a regulated cargo can hold rainwater for another fifteen years. Harvesting, planters, troughs, compost tumblers, ballast, erosion control, aquaponics sumps, dust suppression skids — sixteen standard builds, all from donor stock that failed container service.
And if you do not want it, we will collect it and pay for it. A failed unit is still 55 lb of steel at 92% recovery and 42 lb of HDPE at 68%.
Do I need secondary containment?
That is decided by your cargo and your jurisdiction, not by the container, and it is a question for your own environmental people. Where you do need it, size it for the largest single container plus a margin.
The practical trap is that a spill pallet rated for drums is not rated for an IBC. A 275-gallon tote is 2,420 lb of water or 3,637 lb of 50% caustic, concentrated on thirteen square feet.
How long can I leave a cargo sitting in a tote?
The container is usually not the limit — the cargo is. Hypochlorite loses strength continuously and faster when warm. Hydrogen peroxide off-gasses and needs a vent throughout. Vegetable oils oxidise. Latex is finished if it freezes. Glycols and fertilisers are indefinitely stable.
For the container itself: solid cap, valve closed, out of direct sun, filled to 85% if the cargo is water-based and the temperature will drop below freezing. Under those conditions a sound bottle will sit for years without any change we can measure.
Can I store drinking water in a reclaimed tote?
In a rebottled unit, yes — a new HDPE bottle in an inspected cage, with an FDA-compliant EPDM gasket and new closures. For potable water that is the only option we will sell you.
Not in a washed unit, however good the wash. The bottle has a history, and for drinking water the correct answer to 'what was in it before?' is 'nothing'. Keep it out of sunlight, use it within a season, and treat the water as your own responsibility rather than the container's.
Is a tote safe for diesel or heating oil?
The container handles it: HDPE is good with diesel and a Viton gasket is correct — never EPDM, which swells in hydrocarbons. The constraint is almost never the tote.
It is your local fire code, insurer and state environmental rules, which often restrict storing fuel in a non-metallic container, require secondary containment, or cap the volume on site. Check before you buy, because the container will arrive compliant and the installation may not be.
The twenty-two point intake inspection.
| # | Check | Pass criterion | Fail consequence |
|---|---|---|---|
| 01 | Prior-contents declaration present | Named product, filler, fill date | Quarantine bay until named, or refused |
| 02 | Cargo against exclusion list | Not on the published list | Refused at the gate, load turned away |
| 03 | Residual heel volume | Under 1 gal, drainable | Charged back, or refused above 5 gal |
| 04 | Odour, cap off, ambient | No detectable cargo odour after rinse | Drops to Grade C or reclaim |
| 05 | Bottle wall thickness, four points | Within 15% of nominal | Reclaim |
| 06 | Crazing under raking light | No branching cracks anywhere | Reclaim — crazing never improves |
| 07 | Stress whitening at the sump | None, or faint and non-progressive | Grade C maximum |
| 08 | Bulge, measured at mid-wall | Under 6 mm from datum | Grade C or reclaim by severity |
| 09 | UV chalking on the sun face | Surface only, no wall loss | Grade C for outdoor-only use |
| 10 | Neck thread condition | Clean start, two full turns by hand | Rebottle or reclaim |
| 11 | Internal scope, 360° | No film, no deposit, no shadowing | Re-wash, then regrade |
| 12 | Weld node count and integrity | 44–54 nodes, none cracked | Cage repair or scrap the cage |
| 13 | Cage geometry, diagonal check | Within 10 mm across diagonals | Press back or scrap |
| 14 | Galvanising condition | No red rust through the zinc | Grade C, or wire-brush and paint |
| 15 | Base weld to pallet | All welds sound under load | Scrap the base, transplant the bottle |
| 16 | Pallet type and ISPM stamp | Matches order; stamp present if export | Re-sorted to the correct bay |
| 17 | UN plate legible | All fields readable, dates in date | Sold as non-regulated service only |
| 18 | Leak test, pneumatic decay | Under 1 kPa loss in 10 min at test pressure | Repair and retest, or reclaim |
| 19 | Valve function, full travel | Opens, closes, seals dry | Valve replaced |
| 20 | Gasket condition | Not reused on A or B — always new | New gasket fitted |
| 21 | Photographs, four plus cage stamp | In focus, bay number visible | Reshot before despatch |
| 22 | Passport record written | Cage ID, grade, route, dates, operator | Unit does not leave the yard |
Checks 05 to 09 are where most units lose a grade, and they are all condition of the bottle rather than cleanliness. A container can be surgically clean inside and still be Grade C because of what five Michigan winters did to the outside.
What actually moves the price of a reclaimed tote.
| Driver | Direction | Typical effect | Can you control it? |
|---|---|---|---|
| Grade | A costs more than C | Up to 3× across the range | Yes — most buyers over-specify |
| Wash route required | Route 3 over Route 1 | +18 to +30% | Yes, by naming the real end use |
| New bottle (rebottled) | Up | +40 to +60% over washed | Yes — only food and potable truly need it |
| Quantity against trailer fit | 20, 40, 60 are efficient | ±15% on delivered cost | Yes, and this is the easiest saving |
| Freight zone and lane | Lane beats distance | ±40% on delivered cost | Partly — ask which day we run your lane |
| Season | B and C peak in spring | +15 to +20% March–May | Yes, if your timing is flexible |
| Pallet base specified | Steel or composite over timber | +4 to +20% on the base | Yes |
| New valve and cap | Up | Fixed per unit | Yes — reconditioned hardware is an option on C |
| UN plate in date | Up | +8 to +12% | Only if your cargo is regulated |
| Resin and scrap steel index | Both directions | Moves the whole market | No |
| Diesel | Up with fuel | Freight line only | No |
| Take-back credit on your old units | Down, against the invoice | Offsets part of the order | Yes — ask before you dispose |
We quote containers and freight as separate lines, because a single delivered number hides which of these twelve things you are actually paying for. If a quote you are comparing does not split them, ask.
Reference answers on impact.
What is the single biggest impact in the whole chain?
Making the container in the first place. Everything else — washing, freight, our yard electricity, the fleet — is small against the cradle-to-gate impact of 42 lb of virgin HDPE and 86 lb of virgin steel.
Which means the highest-leverage decision in this entire industry is not which supplier you buy from. It is whether the container you are about to buy needs to be new, and for most cargo the honest answer is no.
Does freight cancel out the benefit?
Not remotely, at the distances involved. At 0.40 kg CO₂e per mile for a trailer carrying twenty units, a 500-mile delivery is about 10 kg CO₂e per container. Avoiding one new tote is in the region of 150 kg CO₂e.
It matters at the margins, which is why we run six scheduled lanes and chase backhaul utilisation — 41% of our return legs are loaded. But no plausible freight distance in the lower 48 makes reuse the worse option.
What happens to the parts you cannot reuse?
HDPE goes to flake at 68% recovery after label and residue loss. Steel is baled and mill-confirmed at 92%. Contaminated fractions go to energy recovery — 535 units' worth in 2025, 1.4% of intake.
The genuine residual is gaskets, labels, adhesive and wash sludge: 4.4% of intake by unit count, 61,428 lb by weight. We publish it rather than rounding it away, and the weight comes from the scale rather than from a unit count.
How do you calculate avoided emissions?
Mass times factor, with every factor published. A reused container avoids the cradle-to-gate impact of the new one it displaced: 42 lb of HDPE at 1.86 kg CO₂e per lb, 55 lb of steel at 0.86, 31 lb of steel pallet at the same, less the 2.3 kg CO₂e of the wash cycle and the freight at 0.40 kg CO₂e per mile.
Where a published range exists we use the end that makes our own numbers look worse — 1.86 against a range up to 2.4 for HDPE, for example. That systematically understates our impact, which is the direction we would rather be wrong in.
Why do you publish a landfill figure?
Because a diversion rate without a residual figure is a marketing number. Ours was 94.2% diverted and 4.4% to landfill in 2025 — gaskets, labels, adhesive and wash sludge, 61,428 lb of it, weighed on the yard scale.
If a supplier quotes you a diversion percentage and cannot immediately tell you what the residual was and what it consisted of, the percentage is not measured. It is estimated, and estimates in this industry drift upward.
Is reuse really better than recycling?
By a wide margin, for this product. Recycling a tote recovers 68% of the HDPE and 92% of the steel and then spends energy turning flake back into a product. Reusing it spends 2.3 kg CO₂e on a wash and keeps 100% of both materials doing the job they were made for.
That is why our disposition table reads 61.4% resold as containers and 18.9% reconditioned, with recycling at 7.2%. Recycling is what we do when reuse has genuinely been exhausted, not as a first resort with a better story attached.
What is the water footprint of a wash?
11.5 gallons of fresh water per container, metered across 2025 and across all four routes, because the rinses cascade and 86% of bay water recirculates.
Against that, making the HDPE bottle it displaced would have used about 4.1 gallons per pound of process water on the low end of the published range — roughly 172 gallons for a 42 lb bottle — plus 1.2 gallons per pound for 86 lb of steel. The wash is not close to being the expensive part.
How the container in your yard came to be shaped like that.
The modern caged IBC is a surprisingly young object, and almost every feature of it is the fossil of a specific problem.
Drums and nothing between
Liquids moved in 55-gallon drums or in bulk tankers. Anything in between meant handling dozens of drums, which is why the intermediate category was invented at all.
The first rigid composites
A blow-moulded plastic bottle inside a steel frame, sized to a pallet footprint so a forklift could handle it. The idea has not changed since.
The pallet footprint settles
40 × 48 inches in North America, 1,200 × 1,000 mm in Europe. Every trailer count on this site descends from that choice.
UN performance testing
Packagings began to be approved by design type and performance test rather than by prescription, which is where the 31HA1 marking family comes from.
Periodic testing arrives
The 2.5-year leak test and 5-year inspection cycle formalised, creating the date-stamped plate that decides whether a used unit can still carry a regulated cargo.
Reconditioning becomes a trade
Enough units in circulation, and enough value in a steel cage that outlasts three bottles, for washing and rebottling to be businesses rather than favours.
One bay and a used pressure washer
Re:IBCtote starts in a rented bay in metro Detroit, washing totes for local chemical blenders who could not get a straight answer about prior contents.
Grading gets published
We write down the disqualifiers rather than keeping them in an inspector's head, because the arguments about Grade B were taking more time than the washing.
The passport
Every unit gets a record keyed to its cage ID: intake, wash parameters, test results, grade, operator, dates. Seven-year retention, reissuable years later.
38,210 containers
Our largest year: 94.2% diverted, 4.4% residual published rather than rounded away, 4,281 tonnes of CO₂e avoided on factors we publish in full.
The same containers, different weather.
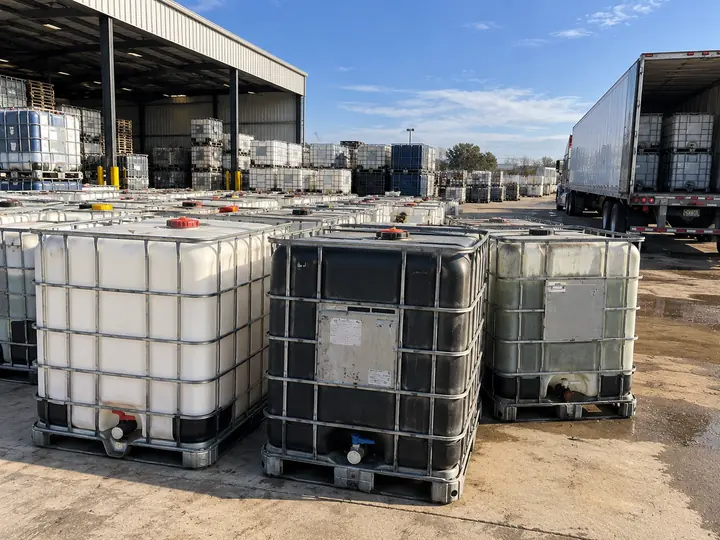
“An inspector who knows the photograph goes to the customer grades more conservatively. We started photographing every unit to end an argument, and it turned into the best quality control we have.”
Send us the cargo, not the grade.
Tell us what is going in the container and what you are doing with it, and we will name the grade, say what would disqualify a unit from it, and tell you if something cheaper does the job. That last part is why people come back.
Where to read next.
Something here is wrong, or missing?
Several of these articles exist because a customer asked a question we could not answer in two sentences. Tell us what you want explained.