Hydrostatic or pneumatic? How leak testing actually works.
A practical explanation of the test that stands between a reconditioned container and a spill.
Ask about this article
Every Grade A and B unit we sell has been leak tested, and the test record is part of what ships with it. Here is what that test is, how the two methods differ, and what a record should contain.
Pneumatic pressure decay
The container is sealed, pressurised with air to a specified low pressure, allowed to stabilise, and then monitored. If the pressure falls faster than the allowed rate over the hold period, it leaks.
**Advantages.** Fast — a cycle takes minutes rather than the better part of an hour. Dry, so the container does not need drying afterwards, which matters enormously for throughput. Very sensitive: a pressure-decay test will find a leak far smaller than hydrostatic will, because gas escapes through paths that liquid will not enter.
**Disadvantages.** Compressed gas stores energy. A container that fails catastrophically under pneumatic test releases that energy suddenly, which is why pneumatic testing happens behind a barrier with nobody standing over it. The pressures involved for IBCs are low, which keeps this manageable, but the principle stands.
**The temperature trap.** Gas pressure varies with temperature. A container filled with air from a compressor is warmer than ambient and will cool during the hold, and that cooling looks exactly like a leak. Stabilisation time before the measurement window is not optional, and a test record without a stabilisation period is not a test record.
Hydrostatic
The container is filled with water, pressurised, and held. Leakage shows as visible water, a measurable drop in level, or a pressure fall.
**Advantages.** Essentially no stored energy — water is incompressible, so a failure is a leak rather than a release. It also tests the container under something very close to real service loading, which pneumatic does not: a full container of liquid has hydrostatic head that an air-filled one does not.
**Disadvantages.** Slow. Water handling. The container has to be dried afterwards, which for a food-grade unit means a complete drying cycle. And it is less sensitive to very small leaks, because surface tension prevents water entering fine paths that air passes through freely.
Which one, and when
For routine periodic leak testing of composite IBCs, pneumatic pressure decay is the standard approach and it is what we run. It is faster, more sensitive, dry, and entirely adequate for the requirement.
Hydrostatic comes out for three cases: when a design type or a customer specification calls for it; after a structural repair where we want the unit loaded the way service will load it; and on steel and stainless bins, where the pressures and the consequences are different.
What a test record should contain
If you are handed a leak test certificate, these are the fields that make it meaningful.
- Container identity — serial or cage ID, not just 'twelve units'
- Method — pneumatic decay or hydrostatic
- Test pressure
- Stabilisation period before the measurement window
- Hold time and the allowable decay criterion
- Measured result, as a number, not as 'pass'
- Ambient temperature
- Date, equipment identity and calibration status
- Operator
A certificate that says 'leak tested: pass' and nothing else is a piece of paper, not evidence. We have seen plenty.
What the test does not tell you
Worth being clear about. A leak test confirms the container holds under the test conditions on the test day. It does not predict crazing, it does not assess chemical compatibility with your cargo, it does not evaluate cage structural condition, and it does not say anything about cleanliness.
Those are four separate checks and a complete reconditioning process includes all of them. The leak test is the last gate, not the whole process.
Calibration, briefly
Our rigs are calibrated quarterly against a traceable reference. This is the least glamorous sentence on this website and it is the one that makes everything above mean anything, because an uncalibrated pressure transducer produces confident numbers that are wrong.
The grading system, in one table.
| Grade | Prior cargo | Wash route | Clean index | Price index | Drops a grade if |
|---|---|---|---|---|---|
| A — Food | One, food only, documented | Route 3 potable triple rinse | 100 | 100 | More than one cargo, missing declaration, film on scope, odour fail |
| A — Rebottled | None — new bottle | New, unused | 98 | 86 | Cage fails node inspection or leak test |
| A — Washed | Non-hazardous industrial | Route 2 hot caustic | 92 | 74 | Ghosting remains, or cargo history unverifiable |
| B — Rinsed | Mixed industrial | Route 1 rinse | 72 | 52 | Structural repair, or odour a buyer would notice |
| C — Non-potable | Heavier residue, repaired | Route 1 rinse | 48 | 34 | Any crazing, any persistent bulge, failed leak test |
| D — Reclaim | Failed test or structure | Not resold | 16 | 9 | Not applicable — this is the floor |
Price index is relative to Grade A food at 100, not a quote. The absolute level moves with resin, scrap steel, freight rates and the agricultural season.
Baseline specifications for everything we handle.
| Container | Capacity | Footprint | Height | Tare | Gross at SG 1.0 | Per 53' trailer |
|---|---|---|---|---|---|---|
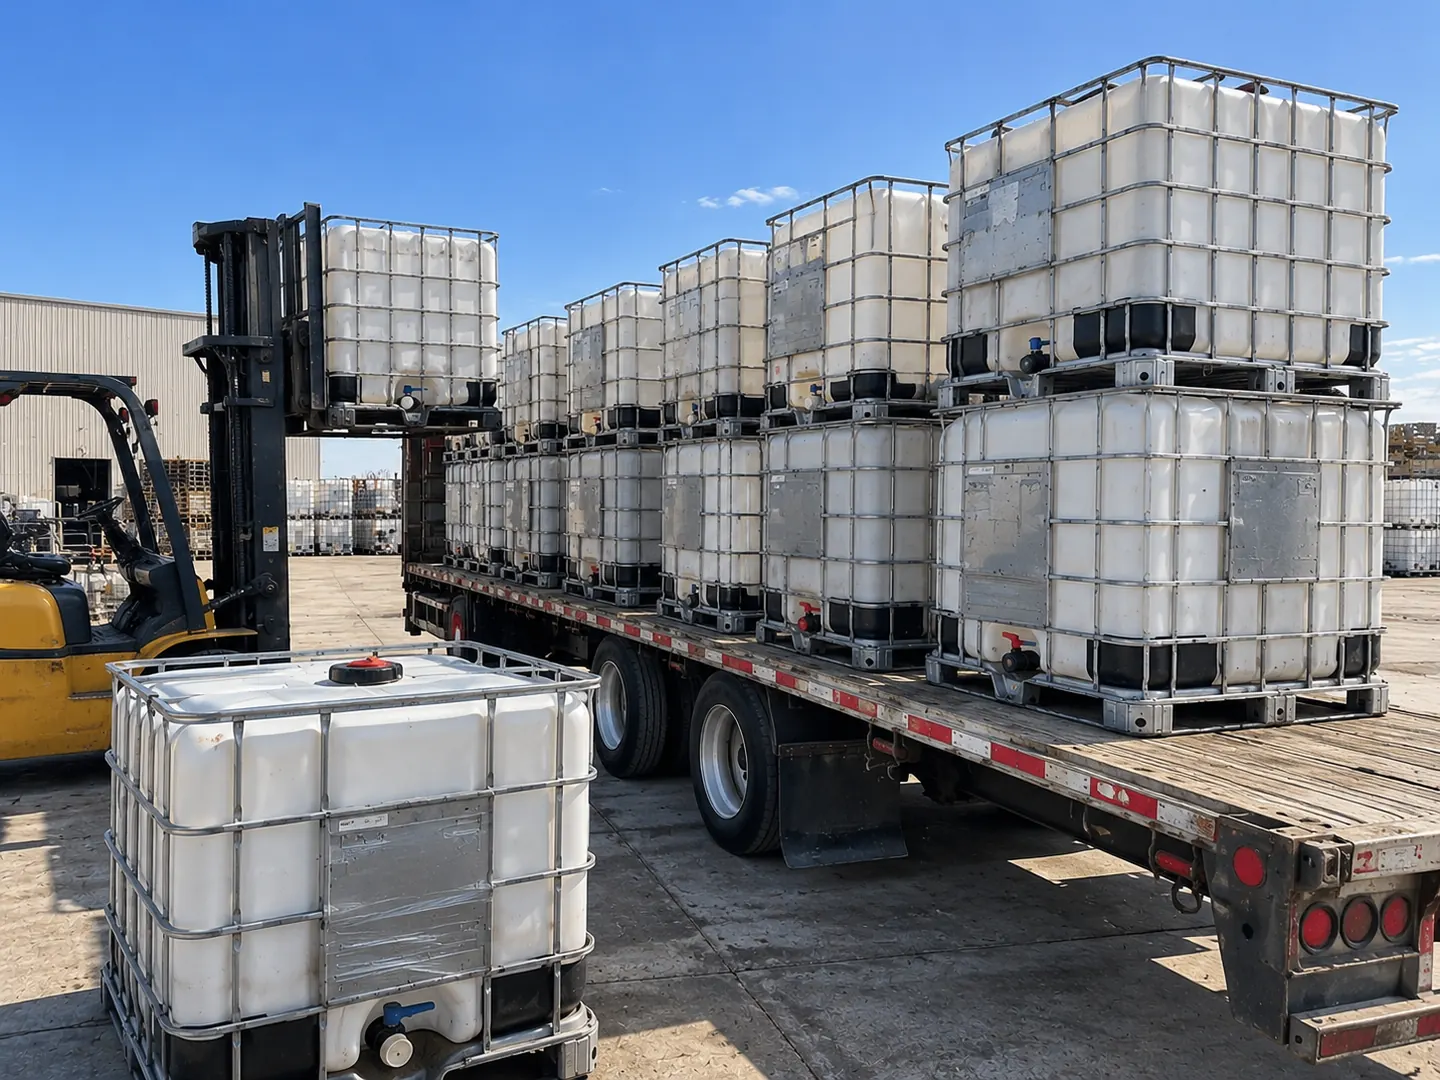
| Caged composite IBC | 275 gal / 1,040 L | 40 × 48 in | 46 in | 127 lb | 2,420 lb | 20 floor / 40 stacked |
| Caged composite IBC, XL | 275 gal / 1,040 L | 40 × 48 in | 53 in | 132 lb | 2,425 lb | 20 / 40 |
| Caged composite IBC | 330 gal / 1,250 L | 40 × 48 in | 53 in | 145 lb | 2,900 lb | 20 / 40 |
| Caged composite IBC | 350 gal / 1,325 L | 48 × 48 in | 52 in | 170 lb | 3,090 lb | 18 / 36 |
| Stainless bin, 304 | 350 gal / 1,325 L | 48 × 42 in | 55 in | 420 lb | 3,340 lb | 18 / — |
| Stainless bin, 316L | 500 gal / 1,893 L | 52 in dia. | 74 in | 580 lb | 4,750 lb | 14 / — |
| Poly drum, closed head | 55 gal / 208 L | 23 in dia. | 34.5 in | 22 lb | 480 lb | 80 on pallets |
| Steel drum, lined | 55 gal / 208 L | 22.5 in dia. | 33.5 in | 38 lb | 496 lb | 80 on pallets |
| Salvage overpack | 95 gal / 360 L | 28 in dia. | 40 in | 35 lb | 827 lb | 40 on pallets |
Figures are nominal and vary a little by moulder. Always multiply net volume by the actual specific gravity of your cargo before checking a forklift or racking rating.
The yard, this month.
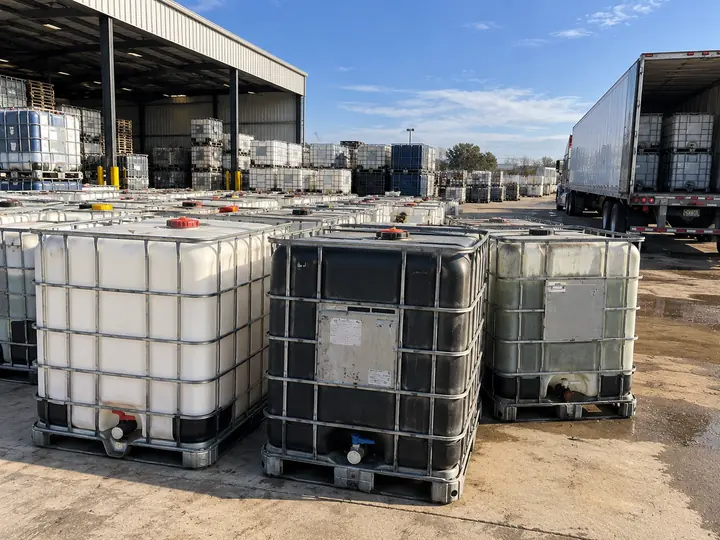
We photograph every unit before despatch, and we photograph the yard because a supplier who will not show you their own concrete is telling you something.
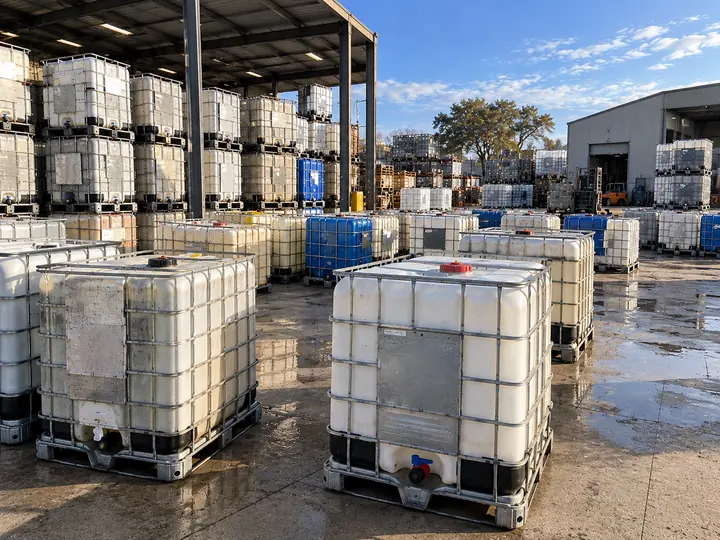
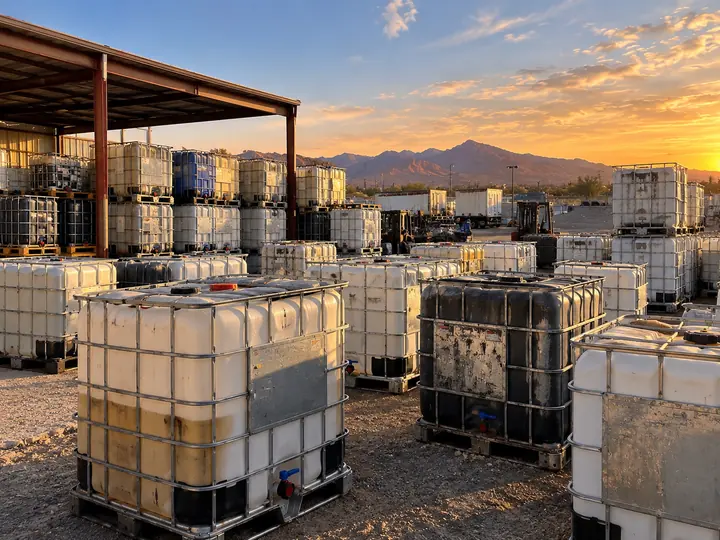
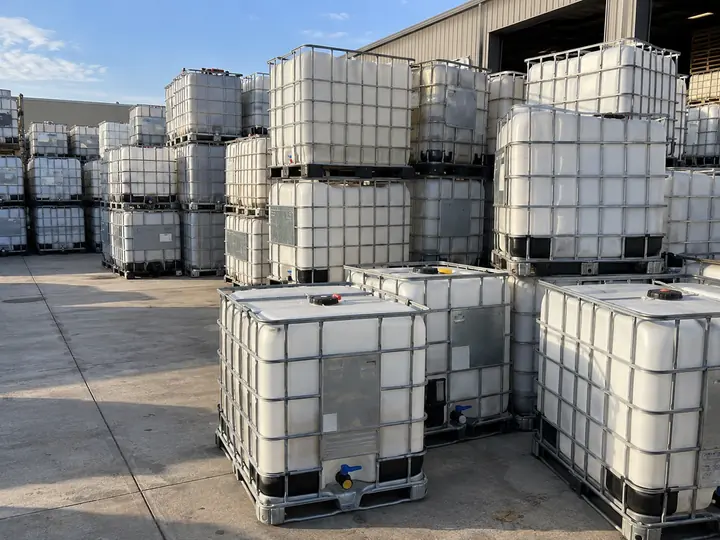
What arrives with the containers.
None of this is optional or chargeable. It is the difference between a reclaimed container and an anonymous second-hand one.
- A prior-contents sheet naming the product, the fill date and the company that filled it
- Four photographs of the actual unit plus an image of the cage stamp
- The grade assigned, and the published criteria that grade commits us to
- A wash record where the unit went through Route 2, 3 or 4, with temperature, dwell, rinse count and final rinse conductivity
- A leak test record for every Grade A and Grade B unit: method, pressure, hold time and measured decay
- The UN plate photograph and periodic test dates where the unit is marked
- A component list naming gasket material, valve type and cap type
- The cage passport ID, so the whole service history can be reissued later
- An allergen flag where a prior food cargo included dairy, egg or tree-nut oils
- A standing take-back offer: when you are finished, we collect and pay
The pages our own staff keep open.
The twelve-minute check to run when the truck arrives.
Do this before the driver leaves, with the paperwork in your hand. It takes about a minute a unit on a small order and it is the only moment when a problem costs you nothing to raise.
Before anything comes off the trailer
- Count the units and compare against the bill of lading, not against memory.
- Photograph the load in the trailer, from the door, before the first unit moves. This single photograph settles almost every freight-damage dispute.
- Look along the top of the load for crushed cages, which is what a stacked load that shifted looks like.
On each unit, as it lands
- Read the cage stamp and check it against the photographs you were sent. Same unit, or not.
- Cap on and tight? A missing or loose top cap means the unit travelled open.
- Dust cap on the discharge? If it is missing, the valve has been exposed to road spray.
- Open and close the valve through full travel, then wipe it dry and watch it for a minute.
- Look along the lower corners and the sump under a raking light for whitening or cracks.
- Check the diagonals by eye: a cage out of square has been hit.
- Look at the base welds, all four corners, with the unit lifted a couple of inches.
- Read the UN plate and confirm the periodic dates match what you ordered, if your cargo is regulated.
On the paperwork, before you sign
- Prior-contents sheet present, naming product, filler and fill date.
- Grade stated, and the wash record attached if it was Route 2, 3 or 4.
- Leak test record present for every A and B unit, with actual numbers on it.
- Gasket material named on the component list, and matching your cargo.
If something is wrong
Note it on the delivery paperwork before signing and photograph it with the unit's cage stamp in the same frame. Then email us. With a cage ID and a photograph we can pull the intake record, the wash log, the leak test and the despatch photographs within minutes, and the conversation is about facts rather than recollection. Units that are not as described come back on our freight, not yours.
Chemical compatibility, container by gasket.
| Cargo | HDPE bottle | EPDM | Viton | PTFE | Note |
|---|---|---|---|---|---|
| Water, potable | Excellent | Excellent | Excellent | Excellent | Rebottled or Grade A food only |
| Sodium hypochlorite 12.5% | Good | Fair | Good | Excellent | Vent — the cargo off-gasses and will bulge a sealed bottle |
| Caustic soda 50% | Excellent | Excellent | Good | Excellent | SG 1.53 — 275 gal only, check the forklift plate |
| Sulphuric acid 93% | Not suitable | Not suitable | Fair | Excellent | Lined steel or stainless service, never poly |
| Hydrochloric acid 35% | Good | Not suitable | Excellent | Excellent | Viton only; HCl destroys EPDM in weeks |
| Nitric acid 10% | Fair | Not suitable | Good | Excellent | Oxidiser — embrittles HDPE over months |
| Phosphoric acid 75% | Good | Fair | Good | Excellent | Common fertiliser intermediate |
| Propylene glycol | Excellent | Excellent | Excellent | Excellent | The most-handled tote cargo in the Midwest |
| Ethylene glycol | Excellent | Excellent | Excellent | Excellent | Label clearly — it is routinely confused with PG |
| Ethanol, 190 proof | Good | Fair | Excellent | Excellent | Flammable — conductive container and bonding required |
| Methanol | Good | Fair | Excellent | Excellent | Permeates slowly through HDPE; not for long storage |
| Mineral oil, white | Excellent | Not suitable | Excellent | Excellent | EPDM swells in hydrocarbons |
| Used motor oil | Excellent | Not suitable | Excellent | Excellent | Warm to 60 °F before pumping in winter |
| Diesel and heating oil | Good | Not suitable | Excellent | Excellent | Check local rules before storing fuel in an IBC |
| Vegetable and canola oil | Excellent | Good | Excellent | Excellent | Hot wash route afterwards or it polymerises |
| Urea solution 32.5% (DEF) | Excellent | Excellent | Excellent | Excellent | Freezes at 12 °F, expands, then recovers |
| Liquid fertiliser 28-0-0 | Excellent | Excellent | Excellent | Excellent | Stains the bottle; does not harm it |
| Ferric chloride 40% | Excellent | Not suitable | Excellent | Excellent | Permanent orange staining — cosmetic only |
| Hydrogen peroxide 35% | Fair | Not suitable | Good | Excellent | Vented cap mandatory; dedicated bottle, never reused |
| Acetic acid 80% | Good | Fair | Good | Excellent | Odour carries over — dedicate the unit |
| Latex paint and coatings | Excellent | Good | Excellent | Excellent | Never let it dry inside; a cured film is unremovable |
| Toluene, xylene, MEK | Not suitable | Not suitable | Good | Excellent | Aromatic solvents swell and soften HDPE |
| Isocyanates and polyols | Refused | Refused | Refused | Refused | On our published exclusion list — they cure |
| Firefighting foam concentrate | Refused | Refused | Refused | Refused | PFAS risk; we will not take it at any price |
Ratings are for ambient-temperature storage in a reclaimed container, not for pressurised or heated service. Every 20 °F above 100 °F roughly halves the service life of the rating. When the cargo is not on this list, send us the SDS and we will tell you what we would and would not put it in.
Cold weather: what freezing actually does, and the four rules.
We are in Livonia, Michigan. We see what winter does to containers every year, and almost all of the damage is avoidable with four decisions made in October rather than January.
What freezing does
Water expands about nine percent when it freezes, and it does not expand evenly — it grows from the coldest surfaces inward, which in a tote means from the walls toward a shrinking core of liquid. The pressure goes somewhere, and in an HDPE bottle it goes to the thickest, most restrained geometry: the lower corner next to the sump. That is why the crack is almost always in the same place, and why it usually appears on thaw rather than on freeze.
Rule one — fill water-based cargo to 85%
Leave the top sixteen percent of a 275 empty and the ice has somewhere to grow. This one decision prevents the great majority of freeze cracks we see. For a 275-gallon tote that is about 234 gallons, and the ribbing on most bottles gives you a usable visual mark at roughly the right height.
Rule two — never forklift a cold full tote hard
Below about −20 °F, HDPE is brittle rather than tough. The same impact that leaves a white mark in July cracks the wall in February. Slow approach, square entry, no dropping the last inch.
Rule three — solid cap, and a drain path
A vented cap in winter is a condensation pump: it breathes moist air in on every temperature cycle, and that water collects on top of the cargo. Solid cap for storage and transit. Store the unit where meltwater can drain away from the base rather than freezing around it, because ice around a steel base is how galvanising gets breached.
Rule four — warm the product, never the bottle
Cold cargo is a viscosity problem, not a blockage. Used motor oil wants to be above about 60 °F before you try to pump it. Warm the product in a heated space or with a blanket rated for IBC use; never apply direct flame, a torpedo heater pointed at the wall, or anything that puts a hot spot on the HDPE. Heat-affected plastic does not recover, and a bottle that has been locally overheated will fail later with no visible warning.
The cargo-specific cases
DEF (urea 32.5%) freezes at 12 °F, expands, and recovers its specification on thaw if it was not overheated — the container is the fragile part, not the fluid. Sodium hypochlorite loses strength steadily at any temperature and faster warm, so winter storage is actually kind to it. Latex products are finished if they freeze. Glycols are fine, which is rather the point of them.
Twenty on the floor, straps across.
Reference answers on specification.
Is stress whitening the same as crazing?
No, and the distinction is worth money. Stress whitening is localised opacity where the polymer has been strained, almost always a forklift impact near the sump. It looks alarming and is often not a failure.
Crazing is a network of fine branching cracks from chemical and mechanical stress together. It is an absolute disqualifier, it never improves, and the test is a raking light at a shallow angle across the surface. If you can see branching, the bottle is finished — though the cage and base are still worth money.
Can a cage be reused with a new bottle?
Yes, and that is what rebottling is: a new blow-moulded HDPE bottle fitted into an inspected cage and base. Cages outlast bottles about three to one, which is why the trade exists.
The cage goes through the same inspection as everything else first — 44 to 54 weld nodes counted individually, diagonals measured, base welds loaded, galvanising checked at the welds. We fitted 4,118 new bottles in 2025. Bench turnaround on contract work is 48 hours.
Do you have 350 and 500 gallon containers?
Yes, as stainless bins rather than caged composites. A 350-gallon square 304 bin is 48 × 42 inches and 55 inches tall with a 420 lb tare; a 500-gallon cylindrical 316L is 52 inches in diameter, 74 tall, 580 lb.
They are the right answer for aggressive acids above SG 1.6, for hot cargo, and for anything where you want a container that will outlive several poly ones. They do not stack, and the trailer count drops to fourteen for the 500s.
What is the heaviest cargo you would put in a reclaimed poly tote?
In practice, 50% caustic soda at SG 1.53 in a 275 — which grosses 3,637 lb — is about where we stop being comfortable, and we check the customer's forklift rating before quoting it.
Sulphuric acid at 93% and SG 1.83 we will not put in poly at all; that is steel or stainless service. The limiting factor is rarely the bottle's burst strength and almost always everything underneath it: forks, beams, floors.
How do I work out whether my cargo is too heavy for a 330?
Multiply litres by specific gravity to get kilograms, or gallons by 8.34 by specific gravity to get pounds, then add the tare — 127 lb for a 275, 145 lb for a 330 — and compare against the maximum gross mass on the UN plate.
The plate figure is the binding one. As a rough guide, cargo above about SG 1.4 belongs in a 275 rather than a 330 simply because the taller bottle puts more mass on the same footprint, and above SG 1.6 you are usually looking at lined steel or stainless rather than poly.
What is the difference between a 275 and a 330, apart from volume?
Height, mostly. Both sit on the same 40 × 48 inch footprint; the 275 is 46 inches tall in the standard build and the 330 is 53. The trailer count is identical at twenty on the floor, which surprises people.
The consequence is density: a 330 full of anything heavy puts more mass on the same square footage, so forklift ratings, racking and floors all need checking against the real figure. For dense cargo, two 275s beat one 330 and a half.
How do I tell which buttress thread I have?
Measure the outside diameter of the male thread: roughly 60 mm is S60×6, 70 mm is S70×6, 75 mm is S75×6. S60×6 is the European norm — Schütz and Werit — and S70×6 covers Mauser and most North American bottles.
The reason this matters is that all three will start on each other and then bind after a turn or two. Two turns and a stop means the wrong standard. Forcing it crazes the bottle neck permanently, and a crazed neck is not repairable.
Washed, or rebottled?
This is the decision that most often gets made on price and should be made on history. The cage and base are the same in both cases — the question is only ever about the bottle.
Washed is right when
- There is a documented prior cargo and it is compatible with your use
- Your cargo is industrial, agricultural or utility
- Food in the same category as the prior cargo, with the declaration in hand
- You want the lower price and the lower embodied impact — nothing new was made
- Ghosting or staining is acceptable: it is cosmetic, and it costs a grade you may not need
- You need units quickly: Route 1 and 2 run at 90 a day
Rebottled is right when
- Drinking water, or any potable application
- Allergen-claim products, infant products, or high-purity and DI water
- An auditor has asked for virgin packaging where it touches the cargo
- The prior cargo cannot be verified, which disqualifies washed stock outright
- You want a plate with a current date and a fresh test clock
- You can wait: bench turnaround is 48 hours on contract work, 3 to 10 days on orders
Symptom, cause, what to do about it.
| Symptom | Most likely cause | Check first | Fix |
|---|---|---|---|
| Weeping at the valve when closed | Seat compression set from long open storage | Close fully, wipe dry, watch 10 min | Replace the valve; store closed in future |
| Drip from under the valve body | Flange gasket, not the valve | Feel behind the valve for wet | Pull the valve, new flange gasket |
| Cargo odour in a clean tote | Original gasket retained, or cap gasket | Smell the gasket itself, off the unit | New gasket; re-rinse; air with the cap off |
| Bottle bulging at mid-wall | Overfill, heat, or off-gassing cargo | Cargo SDS for gas generation; ambient temp | Vented cap at point of use; reduce fill to 85% |
| Condensate on top of the cargo | Vented cap left on in storage | Which cap is fitted | Solid cap for storage; vent only when dispensing |
| Crack at the lower corner | Water-based cargo froze at full fill | Fill level history | Unit is finished — we will take it back for reclaim |
| White cloudy patch at the sump | Stress whitening from forklift impact | Raking light for branching cracks | Monitor; no crazing means serviceable, Grade C |
| Fine branching cracks | Crazing, from chemical stress or UV | Any raking light at a shallow angle | Retire the bottle; the cage and base are reusable |
| Flow stops mid-discharge | Vacuum lock — no air in | Crack the top cap and listen | Vent while dispensing, always |
| Slow flow on a cold morning | Cargo viscosity, not a blockage | Cargo temperature against its SDS | Warm the product; never heat the bottle directly |
| Adapter binds after two turns | Wrong buttress standard | Compare S60×6 / S70×6 / S75×6 | Correct adapter or a proper reducer; never force |
| Cage node cracked | Impact, or a stacked load over rating | Count cracked nodes; check plate stack rating | Do not stack; return for cage swap |
| Tote rocks on the forks | Base weld failed at one corner | Lift 2 in and look at all four welds | Take out of service immediately — transplant job |
| Rust bleeding through the zinc | Galvanising breached, usually at a weld | Wire-brush a test patch | Cosmetic for utility use; fails food-grade intake |
| Label illegible after a season | Direct-print on HDPE in UV | Whether the UN plate is also fading | Stencil and clear-coat, or stainless tag |
Temperature limits and the derating nobody mentions.
| Temperature | HDPE bottle | Steel cage | Gasket | Stacking allowed | Practical effect |
|---|---|---|---|---|---|
| Below −20 °F | Brittle | Fine | Hardened | No | Impact cracking at the sump corner; do not forklift a cold full tote hard |
| −20 to 32 °F | Serviceable | Fine | Stiff | Yes, derate 25% | Water-based cargo freezing; fill to 85% only |
| 32 to 100 °F | Full rating | Full rating | Full rating | Yes, full | Normal service window — every published figure assumes this |
| 100 to 120 °F | Softening | Fine | Fine | Derate 50% | Visible bulge in a full tote standing in July sun |
| 120 to 140 °F | Marginal | Fine | Check cargo | No | Creep accelerates; never stack, never rack |
| 140 to 160 °F | Short excursion only | Fine | EPDM limit | No | Wash bay territory — empty units only |
| Above 160 °F | Not suitable | Fine | PTFE only | No | Permanent deformation; the unit leaves as Grade D |
Heat-affected HDPE does not recover its original wall strength when it cools. This is why anything that has been near a fire is refused at our gate regardless of how it looks.
Reference answers on use.
What can I do with a tote that failed?
A bottle that cannot be trusted with a regulated cargo can hold rainwater for another fifteen years. Harvesting, planters, troughs, compost tumblers, ballast, erosion control, aquaponics sumps, dust suppression skids — sixteen standard builds, all from donor stock that failed container service.
And if you do not want it, we will collect it and pay for it. A failed unit is still 55 lb of steel at 92% recovery and 42 lb of HDPE at 68%.
Do I need secondary containment?
That is decided by your cargo and your jurisdiction, not by the container, and it is a question for your own environmental people. Where you do need it, size it for the largest single container plus a margin.
The practical trap is that a spill pallet rated for drums is not rated for an IBC. A 275-gallon tote is 2,420 lb of water or 3,637 lb of 50% caustic, concentrated on thirteen square feet.
How long can I leave a cargo sitting in a tote?
The container is usually not the limit — the cargo is. Hypochlorite loses strength continuously and faster when warm. Hydrogen peroxide off-gasses and needs a vent throughout. Vegetable oils oxidise. Latex is finished if it freezes. Glycols and fertilisers are indefinitely stable.
For the container itself: solid cap, valve closed, out of direct sun, filled to 85% if the cargo is water-based and the temperature will drop below freezing. Under those conditions a sound bottle will sit for years without any change we can measure.
Can I store drinking water in a reclaimed tote?
In a rebottled unit, yes — a new HDPE bottle in an inspected cage, with an FDA-compliant EPDM gasket and new closures. For potable water that is the only option we will sell you.
Not in a washed unit, however good the wash. The bottle has a history, and for drinking water the correct answer to 'what was in it before?' is 'nothing'. Keep it out of sunlight, use it within a season, and treat the water as your own responsibility rather than the container's.
Is a tote safe for diesel or heating oil?
The container handles it: HDPE is good with diesel and a Viton gasket is correct — never EPDM, which swells in hydrocarbons. The constraint is almost never the tote.
It is your local fire code, insurer and state environmental rules, which often restrict storing fuel in a non-metallic container, require secondary containment, or cap the volume on site. Check before you buy, because the container will arrive compliant and the installation may not be.
Can I use a tote for compost tea or digestate?
Yes, and Grade B rinsed is the right stock for it. The one rule is venting: biological activity generates gas, and a sealed cap on a fermenting cargo will bulge the bottle and eventually deform it permanently.
Fit a vented cap or a breather valve at the point of use, keep the unit out of direct sun to limit the temperature swing, and expect to wash it out between batches rather than at end of season.
What size tote for livestock water?
A 275 on a level bearing pad, Grade B rinsed with a documented prior cargo, black or painted rather than translucent. Translucent bottles grow algae in one season in the open.
Our framed trough build is the better answer if animals have direct access: a half-height open trough, 120 gallons, with the cage left intact as the frame. Full totes should never be where livestock can rub against them — 2,420 lb on four square feet does not need much persuasion to tip.
The twenty-two point intake inspection.
| # | Check | Pass criterion | Fail consequence |
|---|---|---|---|
| 01 | Prior-contents declaration present | Named product, filler, fill date | Quarantine bay until named, or refused |
| 02 | Cargo against exclusion list | Not on the published list | Refused at the gate, load turned away |
| 03 | Residual heel volume | Under 1 gal, drainable | Charged back, or refused above 5 gal |
| 04 | Odour, cap off, ambient | No detectable cargo odour after rinse | Drops to Grade C or reclaim |
| 05 | Bottle wall thickness, four points | Within 15% of nominal | Reclaim |
| 06 | Crazing under raking light | No branching cracks anywhere | Reclaim — crazing never improves |
| 07 | Stress whitening at the sump | None, or faint and non-progressive | Grade C maximum |
| 08 | Bulge, measured at mid-wall | Under 6 mm from datum | Grade C or reclaim by severity |
| 09 | UV chalking on the sun face | Surface only, no wall loss | Grade C for outdoor-only use |
| 10 | Neck thread condition | Clean start, two full turns by hand | Rebottle or reclaim |
| 11 | Internal scope, 360° | No film, no deposit, no shadowing | Re-wash, then regrade |
| 12 | Weld node count and integrity | 44–54 nodes, none cracked | Cage repair or scrap the cage |
| 13 | Cage geometry, diagonal check | Within 10 mm across diagonals | Press back or scrap |
| 14 | Galvanising condition | No red rust through the zinc | Grade C, or wire-brush and paint |
| 15 | Base weld to pallet | All welds sound under load | Scrap the base, transplant the bottle |
| 16 | Pallet type and ISPM stamp | Matches order; stamp present if export | Re-sorted to the correct bay |
| 17 | UN plate legible | All fields readable, dates in date | Sold as non-regulated service only |
| 18 | Leak test, pneumatic decay | Under 1 kPa loss in 10 min at test pressure | Repair and retest, or reclaim |
| 19 | Valve function, full travel | Opens, closes, seals dry | Valve replaced |
| 20 | Gasket condition | Not reused on A or B — always new | New gasket fitted |
| 21 | Photographs, four plus cage stamp | In focus, bay number visible | Reshot before despatch |
| 22 | Passport record written | Cage ID, grade, route, dates, operator | Unit does not leave the yard |
Checks 05 to 09 are where most units lose a grade, and they are all condition of the bottle rather than cleanliness. A container can be surgically clean inside and still be Grade C because of what five Michigan winters did to the outside.
What actually moves the price of a reclaimed tote.
| Driver | Direction | Typical effect | Can you control it? |
|---|---|---|---|
| Grade | A costs more than C | Up to 3× across the range | Yes — most buyers over-specify |
| Wash route required | Route 3 over Route 1 | +18 to +30% | Yes, by naming the real end use |
| New bottle (rebottled) | Up | +40 to +60% over washed | Yes — only food and potable truly need it |
| Quantity against trailer fit | 20, 40, 60 are efficient | ±15% on delivered cost | Yes, and this is the easiest saving |
| Freight zone and lane | Lane beats distance | ±40% on delivered cost | Partly — ask which day we run your lane |
| Season | B and C peak in spring | +15 to +20% March–May | Yes, if your timing is flexible |
| Pallet base specified | Steel or composite over timber | +4 to +20% on the base | Yes |
| New valve and cap | Up | Fixed per unit | Yes — reconditioned hardware is an option on C |
| UN plate in date | Up | +8 to +12% | Only if your cargo is regulated |
| Resin and scrap steel index | Both directions | Moves the whole market | No |
| Diesel | Up with fuel | Freight line only | No |
| Take-back credit on your old units | Down, against the invoice | Offsets part of the order | Yes — ask before you dispose |
We quote containers and freight as separate lines, because a single delivered number hides which of these twelve things you are actually paying for. If a quote you are comparing does not split them, ask.
Reference answers on impact.
What is the water footprint of a wash?
11.5 gallons of fresh water per container, metered across 2025 and across all four routes, because the rinses cascade and 86% of bay water recirculates.
Against that, making the HDPE bottle it displaced would have used about 4.1 gallons per pound of process water on the low end of the published range — roughly 172 gallons for a 42 lb bottle — plus 1.2 gallons per pound for 86 lb of steel. The wash is not close to being the expensive part.
Can I use your numbers in my own reporting?
Yes, and the methodology document exists for that purpose: every factor, its published range, and which end we chose. Several customers put the disposition record for their own returned units into their annual reporting.
We will also tell you what we do not have: no third-party verified LCA, no certification scheme membership, and a solar installation that covers 31% of yard electricity rather than the number we hoped for, because phase two is sitting in a utility interconnection queue. That list is in the vendor pack too.
What is the single biggest impact in the whole chain?
Making the container in the first place. Everything else — washing, freight, our yard electricity, the fleet — is small against the cradle-to-gate impact of 42 lb of virgin HDPE and 86 lb of virgin steel.
Which means the highest-leverage decision in this entire industry is not which supplier you buy from. It is whether the container you are about to buy needs to be new, and for most cargo the honest answer is no.
Does freight cancel out the benefit?
Not remotely, at the distances involved. At 0.40 kg CO₂e per mile for a trailer carrying twenty units, a 500-mile delivery is about 10 kg CO₂e per container. Avoiding one new tote is in the region of 150 kg CO₂e.
It matters at the margins, which is why we run six scheduled lanes and chase backhaul utilisation — 41% of our return legs are loaded. But no plausible freight distance in the lower 48 makes reuse the worse option.
What happens to the parts you cannot reuse?
HDPE goes to flake at 68% recovery after label and residue loss. Steel is baled and mill-confirmed at 92%. Contaminated fractions go to energy recovery — 535 units' worth in 2025, 1.4% of intake.
The genuine residual is gaskets, labels, adhesive and wash sludge: 4.4% of intake by unit count, 61,428 lb by weight. We publish it rather than rounding it away, and the weight comes from the scale rather than from a unit count.
How do you calculate avoided emissions?
Mass times factor, with every factor published. A reused container avoids the cradle-to-gate impact of the new one it displaced: 42 lb of HDPE at 1.86 kg CO₂e per lb, 55 lb of steel at 0.86, 31 lb of steel pallet at the same, less the 2.3 kg CO₂e of the wash cycle and the freight at 0.40 kg CO₂e per mile.
Where a published range exists we use the end that makes our own numbers look worse — 1.86 against a range up to 2.4 for HDPE, for example. That systematically understates our impact, which is the direction we would rather be wrong in.
Why do you publish a landfill figure?
Because a diversion rate without a residual figure is a marketing number. Ours was 94.2% diverted and 4.4% to landfill in 2025 — gaskets, labels, adhesive and wash sludge, 61,428 lb of it, weighed on the yard scale.
If a supplier quotes you a diversion percentage and cannot immediately tell you what the residual was and what it consisted of, the percentage is not measured. It is estimated, and estimates in this industry drift upward.
How the container in your yard came to be shaped like that.
The modern caged IBC is a surprisingly young object, and almost every feature of it is the fossil of a specific problem.
Drums and nothing between
Liquids moved in 55-gallon drums or in bulk tankers. Anything in between meant handling dozens of drums, which is why the intermediate category was invented at all.
The first rigid composites
A blow-moulded plastic bottle inside a steel frame, sized to a pallet footprint so a forklift could handle it. The idea has not changed since.
The pallet footprint settles
40 × 48 inches in North America, 1,200 × 1,000 mm in Europe. Every trailer count on this site descends from that choice.
UN performance testing
Packagings began to be approved by design type and performance test rather than by prescription, which is where the 31HA1 marking family comes from.
Periodic testing arrives
The 2.5-year leak test and 5-year inspection cycle formalised, creating the date-stamped plate that decides whether a used unit can still carry a regulated cargo.
Reconditioning becomes a trade
Enough units in circulation, and enough value in a steel cage that outlasts three bottles, for washing and rebottling to be businesses rather than favours.
One bay and a used pressure washer
Re:IBCtote starts in a rented bay in metro Detroit, washing totes for local chemical blenders who could not get a straight answer about prior contents.
Grading gets published
We write down the disqualifiers rather than keeping them in an inspector's head, because the arguments about Grade B were taking more time than the washing.
The passport
Every unit gets a record keyed to its cage ID: intake, wash parameters, test results, grade, operator, dates. Seven-year retention, reissuable years later.
38,210 containers
Our largest year: 94.2% diverted, 4.4% residual published rather than rounded away, 4,281 tonnes of CO₂e avoided on factors we publish in full.
The same containers, different weather.
“Half the people who ask us for food-grade are about to put site water in it. Telling them so costs us a third of the invoice and earns the next four orders.”
Send us the cargo, not the grade.
Tell us what is going in the container and what you are doing with it, and we will name the grade, say what would disqualify a unit from it, and tell you if something cheaper does the job. That last part is why people come back.