What we are certified for, what we work to, and what we are not.
Container reconditioning is a lightly certified industry, which makes it easy to imply more than is true. Here is the complete, unembellished list.
Quote: Standards & Certifications
Documents we can produce the same day you ask.
UN 31HA1 periodic test capability
In-house leak testing and periodic inspection with calibrated equipment, signed records and re-plating on pass. Test rigs calibrated quarterly against a traceable reference.
Written wash bay SOP
The procedure the bay actually runs to, covering all four wash routes, modelled on RPA reusable-container guidance and 21 CFR 110 sanitation principles.
Municipal discharge permit
Industrial wastewater discharge permit with monthly sampling. Results available to any customer who asks.
General and product liability insurance
Certificate of insurance issued on request as part of a standard vendor onboarding pack.
Seven-year record retention
Wash records, test records, prior-contents declarations and photographs, retrievable against a cage ID or serial.
Hazardous waste generator registration
For the small residual streams we cannot process, handled through licensed partners with manifests retained.
The honest half of this page.
We are a container reconditioner. We are not a food processor, a laboratory, or a certification body, and we do not hold the following — despite several of them being things customers occasionally assume:
- We are not SQF, BRC or FSSC 22000 certified. Those are food manufacturing schemes and we are not a food manufacturer.
- We are not ISO 9001 or ISO 14001 registered. We run documented procedures and publish our environmental figures, but we have not paid for the badge.
- We are not an accredited testing laboratory. Our UN periodic testing is performed to the regulatory requirement with calibrated equipment and signed records, which is what the regulation asks for, but we are not an ISO 17025 lab.
- We do not hold third-party verification of our carbon figures. We get an external desk review each January and we describe it as exactly that.
- We are not a licensed hazardous waste treatment facility. Hazardous residues go to licensed partners.
Why we list this
Because the alternative is a page full of logos and implications, and because every serious buyer eventually asks. Telling you up front what we do not have saves everybody a week.
If a reconditioner's website shows you certification logos without naming the scheme and the scope, ask which legal entity holds it and for what activity. It is a very clarifying question.
What arrives in one email when you onboard us.
- W-9
- Certificate of insurance, general and product liability
- Wash bay standard operating procedure
- Sample wash record and sample leak test record
- Prior-contents declaration template
- Industrial discharge permit number and latest sampling summary
- Impact methodology document
- Written statement of what we are not certified for — the list above, signed
The company in numbers.
| Item | Figure | Note |
|---|---|---|
| Founded | 2009 | One rented bay and a used pressure washer |
| Site | 41,000 sq ft | 11966 Brookfield St, Livonia, MI 48150 |
| Outbound bays | 168 | Numbered and sorted by grade and configuration |
| People | 31 | Including six drivers and two fabricators |
| Containers handled to date | 418,900 | Each with a passport record since 2023 |
| Containers handled in 2025 | 38,210 | Our largest year |
| Fresh water per wash | 11.5 gal | 86% of wash water recirculated |
| Landfill diversion | 94.2% | Residual 4.4% published annually |
| Weld nodes inspected per cage | 44 – 54 | Counted individually, not sampled |
| Photographs per unit | 4 | Plus the cage stamp, before despatch |
| Record retention | 7 years | Reissuable against a cage ID |
| Rooftop solar | 31% of yard electricity | Phase two deferred on a utility queue |
| Road fleet | 6 diesel tractors | 41% backhaul utilisation, averaging 6.4 mpg |
| Telephone lines | 0 | Deliberate; everything in writing |
Documents we will send in one email.
Ask for the vendor pack and all of this arrives together, usually inside the hour.
- W-9
- Certificate of insurance — general and product liability
- Wash bay standard operating procedure, covering all four routes
- Sample wash record and sample leak test record
- Prior-contents declaration template for your own fillers
- Industrial wastewater discharge permit number and latest sampling summary
- Impact methodology document with the full factor table
- A signed statement of what we are NOT certified for — the honest half
- Hazardous waste generator registration details for residual streams
- Record retention policy and how to request a reissue against a cage ID
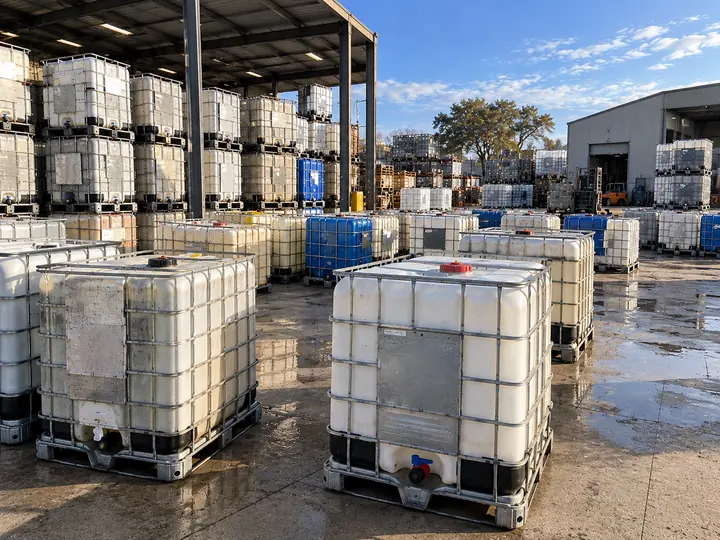
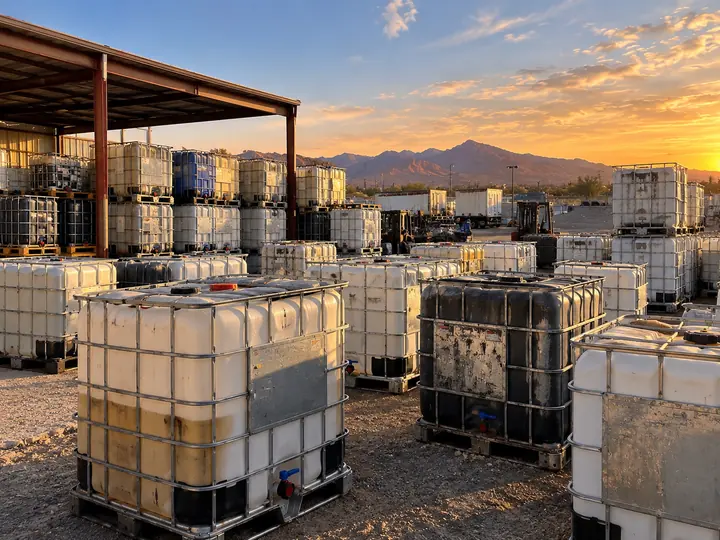
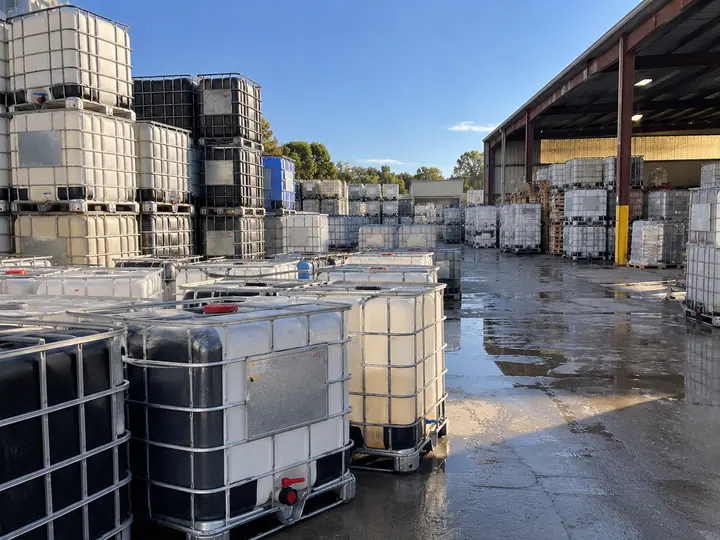
Three frames from the apron.
Grades side by side, plates facing out, and the load plan being executed. This is the whole business in three photographs.
Cargo we will not accept, at any price.
Published because an undeclared container in a recirculating wash system can affect a hundred units before anybody notices. The upside of accepting one is a trailer's margin; the downside is a drained loop and a contaminated batch.
- Pesticides and herbicides — residues persist in HDPE at agronomically significant levels
- Pharmaceutical actives — potent at trace levels with no validatable removal route here
- PFAS-containing formulations, including firefighting foams
- Isocyanates — they cure, and a cured film is a lining no wash removes
- Radiological material
- Anything that has been in a fire — heat-affected HDPE is structurally unpredictable
- Polymerising oils such as tung and linseed
- Any cargo nobody will name in writing, which overrides every other line on this list
What people ask about how we operate.
Why do you publish your landfill figure?
Because a diversion rate without a residual figure is a marketing number. Anybody can say they divert 94% of their material.
Our 4.4% is mostly used gaskets, labels, adhesive residue and wash sludge. Gaskets are the largest contributor by count, they are thermoset, mixed and contaminated, and we genuinely cannot find anyone to take them.
Do you buy carbon offsets?
No, and we do not net anything against anything. Avoided emissions are reported as avoided emissions, separately from our own footprint.
Our trucks burn diesel — six tractors averaging 6.4 mpg. Milk runs and backhaul matching cut the miles per container by about 41%, which is real, but the fuel is still fuel.
Can my old bottles be recycled back into new tote bottles?
Realistically no, and anybody claiming otherwise is being loose with language. Post-industrial container flake carries prior-cargo risk and is not food-contact approved, and tote bottles are a demanding moulding application that wants consistent virgin-grade resin.
Our flake becomes drainage pipe, pallets and agricultural tubing at 68% recovery. Cages and pallets go to a regional electric arc furnace at 92% recovery.
Are your figures third-party verified?
No. The factor table and boundary definition get an external desk review each January by an independent consultant who checks arithmetic and factor sourcing.
That is a desk review, not certified verification, and we describe it that way deliberately. The full methodology, including three stated limitations, is published.
Can I get a certificate for my sustainability report?
Yes, with every take-back collection: unit count, weighed mass, the split between resale, recondition, upcycle and recycle, and estimated CO₂e avoided referenced to the published factor table.
It is a much better figure than 'we recycle our containers', and it survives the question of where the number came from.
Is reusing a container actually better, or is washing it worse?
Better, by roughly thirty to one. A new 275-gallon composite IBC carries about 112 kg CO₂e of embodied impact. A wash cycle costs 2.3 kg CO₂e and 11.5 gallons of fresh water.
Reuse does not reduce embodied carbon; it amortises it. One cage across seven service lives divides the manufacturing impact by seven instead of paying it again each time.
The four wash routes and what each one logs.
| Route | Temperature | Chemistry | Rinses | Verification | Grade produced |
|---|---|---|---|---|---|
| 1 — Rinse only | Ambient to 100 °F | None or mild | 1–2 drained charges | Visual | B — rinsed |
| 2 — Hot caustic | 140–160 °F | Alkaline detergent, dosed | 3 cascade charges | Conductivity + scope | A — washed |
| 3 — Potable triple | 140–160 °F | Food-safe alkaline | 3 full potable charges | Conductivity vs supply + odour | A — food |
| 4 — Customer SOP | As specified | As specified | As specified | Every parameter logged | As agreed |
The route is chosen by prior cargo at the inspection stage, not by price at the sales desk. Fresh water use is 11.5 gallons per unit across all routes because the rinses cascade.
Commercial questions.
Can I specify valve, cap and gasket?
All three, on any grade. If you name the cargo we will specify them for you rather than making you learn three buttress thread standards and six camlock types.
The most expensive eleven-dollar mistake in this industry is EPDM in aromatic service. It swells, extrudes out of the joint and fails without warning.
What payment terms do you offer?
Pro forma for a first order, net 30 on account once established, and purchase orders for public buyers as standard.
Quotes are valid thirty days. Beyond that we refresh rather than honour a stale number, in either direction — this market moves with resin, scrap steel and the agricultural season.
Will you tell me to buy something cheaper?
Frequently, and it is commitment seven of our circular pledge: every new-container quote includes the nearest reclaimed option with the carbon difference written out.
We also steer dense cargo from 330s to 275s, site water from Grade A to Grade C, and drinking water away from used bottles entirely.
What is the minimum order, really?
One unit, on every product line. There is no hidden minimum and no 'pallet quantity only' rule.
Freight is what makes single units expensive. Inside our six weekly lanes we will usually fold one tote into a scheduled route rather than quoting LTL, which is why a single-unit order to Toledo costs a fraction of a single-unit order to Dallas.
Can I see the exact units before paying?
Yes, and it is standard rather than a concession. Four photographs per unit plus the cage stamp, tagged to a bay number, emailed before payment.
This started as a way of ending a recurring argument about Grade B expectations. It turned into our most effective quality control, because an inspector who knows the photograph goes to the customer grades more conservatively.
How do I know the grade is honest?
Because the disqualifiers are published. A Grade A food unit drops to Grade A washed if there is more than one prior cargo, if the declaration is missing, if third-rinse conductivity is out of tolerance, if the scope shows film, or if the odour check fails.
Ask any supplier what would disqualify a unit from the grade they just sold you. A supplier who cannot answer immediately does not have a grading system.
The pages our own staff keep open.
Fourteen stations: what happens between the gate and the truck.
A container that arrives on a Monday morning and leaves as Grade A food on Thursday has been through fourteen stations, and at eight of them it can lose a grade or be pulled out entirely. This is the route, in order.
1 — Gate and declaration
Nothing comes off the trailer without a named prior cargo in writing. No name, no entry; the load goes back. This is the single rule that protects everything downstream, because one undeclared pesticide tote in a recirculating wash loop can affect a hundred units before anybody smells it.
2 — Exclusion screen
The declared cargo is checked against the published exclusion list. Pesticides, pharmaceutical actives, PFAS formulations, isocyanates, radiological material, fire-affected units and polymerising oils are refused outright, whatever the condition and whatever the price.
3 — Heel drain and measure
Residual cargo is drained, measured and routed to the correct waste stream. Under a gallon is normal. Above five gallons the load is a liquid-waste job rather than a container job, and it is priced or refused as one.
4 — Weigh and log
Yard scale, not a unit count. Every published tonnage on this site traces back to this scale, which is why our disposition table reports weight and units separately and why they do not divide into each other neatly.
5 — Cage and base inspection
Node by node, 44 to 54 of them, counted rather than sampled. Diagonals measured. Base welds loaded and watched. Galvanising checked at the welds, which is where it always goes first.
6 — Bottle condition
Wall thickness at four points, raking light across the whole surface for crazing, sump checked for stress whitening, mid-wall measured for bulge against a datum. This is where most grade losses happen, and none of them are about cleanliness.
7 — Wash route assignment
Decided here, by prior cargo, by an inspector — not at the sales desk by price. A food cargo goes to Route 3 whether the customer asked for it or not; an industrial cargo cannot buy its way onto Route 3.
8 — Wash
Route 1 rinse, Route 2 hot caustic, Route 3 potable triple rinse, or Route 4 to a customer's own written SOP. Temperature, dwell, rinse count and chemistry dosing are logged against the cage ID as it happens, not reconstructed afterwards.
9 — Rinse verification
Third-rinse conductivity against the day's measured supply water, final pH, 360-degree internal scope, and an independent two-operator odour check with the cap off. Any one of them failing sends the unit back to station 8.
10 — Hardware
New gasket on every Grade A and B unit, no exceptions. Valve function-tested and replaced if scored. New cap. Adapter threads checked under a light. Tamper seal on anything food-grade.
11 — Leak test
Pneumatic pressure decay on the complete assembly, under 1 kPa loss in ten minutes. Method, pressure, hold time and measured decay are written to the record — a pass with no numbers behind it is not a leak test.
12 — Grade and passport
The grade is assigned against the published criteria and written to the passport with the cage ID, the wash route, the test dates and the operator who did it. Seven years of retention, reissuable on request.
13 — Photography
Four shots of the actual unit plus the cage stamp, bay number visible. These go to the customer before payment. It started as a way of ending arguments about Grade B and became our best quality control, because an inspector who knows the photograph goes out grades more conservatively.
14 — Bay and load plan
Into one of 168 numbered bays by grade and configuration, then load-planned against trailer capacity. Twenty on the floor, forty double-stacked empty. If your order is twenty-two units, this is the station where somebody emails you to suggest twenty or forty.
The twenty-two point intake inspection.
| # | Check | Pass criterion | Fail consequence |
|---|---|---|---|
| 01 | Prior-contents declaration present | Named product, filler, fill date | Quarantine bay until named, or refused |
| 02 | Cargo against exclusion list | Not on the published list | Refused at the gate, load turned away |
| 03 | Residual heel volume | Under 1 gal, drainable | Charged back, or refused above 5 gal |
| 04 | Odour, cap off, ambient | No detectable cargo odour after rinse | Drops to Grade C or reclaim |
| 05 | Bottle wall thickness, four points | Within 15% of nominal | Reclaim |
| 06 | Crazing under raking light | No branching cracks anywhere | Reclaim — crazing never improves |
| 07 | Stress whitening at the sump | None, or faint and non-progressive | Grade C maximum |
| 08 | Bulge, measured at mid-wall | Under 6 mm from datum | Grade C or reclaim by severity |
| 09 | UV chalking on the sun face | Surface only, no wall loss | Grade C for outdoor-only use |
| 10 | Neck thread condition | Clean start, two full turns by hand | Rebottle or reclaim |
| 11 | Internal scope, 360° | No film, no deposit, no shadowing | Re-wash, then regrade |
| 12 | Weld node count and integrity | 44–54 nodes, none cracked | Cage repair or scrap the cage |
| 13 | Cage geometry, diagonal check | Within 10 mm across diagonals | Press back or scrap |
| 14 | Galvanising condition | No red rust through the zinc | Grade C, or wire-brush and paint |
| 15 | Base weld to pallet | All welds sound under load | Scrap the base, transplant the bottle |
| 16 | Pallet type and ISPM stamp | Matches order; stamp present if export | Re-sorted to the correct bay |
| 17 | UN plate legible | All fields readable, dates in date | Sold as non-regulated service only |
| 18 | Leak test, pneumatic decay | Under 1 kPa loss in 10 min at test pressure | Repair and retest, or reclaim |
| 19 | Valve function, full travel | Opens, closes, seals dry | Valve replaced |
| 20 | Gasket condition | Not reused on A or B — always new | New gasket fitted |
| 21 | Photographs, four plus cage stamp | In focus, bay number visible | Reshot before despatch |
| 22 | Passport record written | Cage ID, grade, route, dates, operator | Unit does not leave the yard |
Checks 05 to 09 are where most units lose a grade, and they are all condition of the bottle rather than cleanliness. A container can be surgically clean inside and still be Grade C because of what five Michigan winters did to the outside.
Rinse verification: the numbers behind a wash record.
| Measurement | Method | Pass tolerance | What it actually proves |
|---|---|---|---|
| Third-rinse conductivity | Inline probe, µS/cm | Within 10% of supply water | No dissolved residue carrying over |
| Supply water baseline | Measured each shift | Logged, not assumed | The comparison has a real datum |
| pH of final rinse | Probe | 6.5 – 8.0 | Caustic or acid fully flushed |
| Visual, 360° internal scope | Borescope on a mast | No film, no shadow, no deposit | Nothing clinging above the heel line |
| Odour, cap off, ambient | Two operators independently | Neither detects cargo | The check a buyer will make themselves |
| Wash temperature | Bay thermocouple, logged | Route 2 and 3: 140–160 °F | The chemistry ran where it works |
| Dwell time | Cycle timer, logged | Per route specification | Not a quick splash through |
| Rinse count | Counted charges, logged | Route 3: three full potable | Dilution did the work, not optimism |
| Drain-down | Inverted dwell | Under 100 ml retained | No pooled water to go stale in storage |
| Leak test after wash | Pneumatic pressure decay | Under 1 kPa in 10 min | The wash did not find a weakness |
Conductivity against the day's supply water is the measurement that matters, and it is the one most wash records leave out. A number with no baseline is decoration. Ask any supplier what their third rinse read and what the tap read that morning.
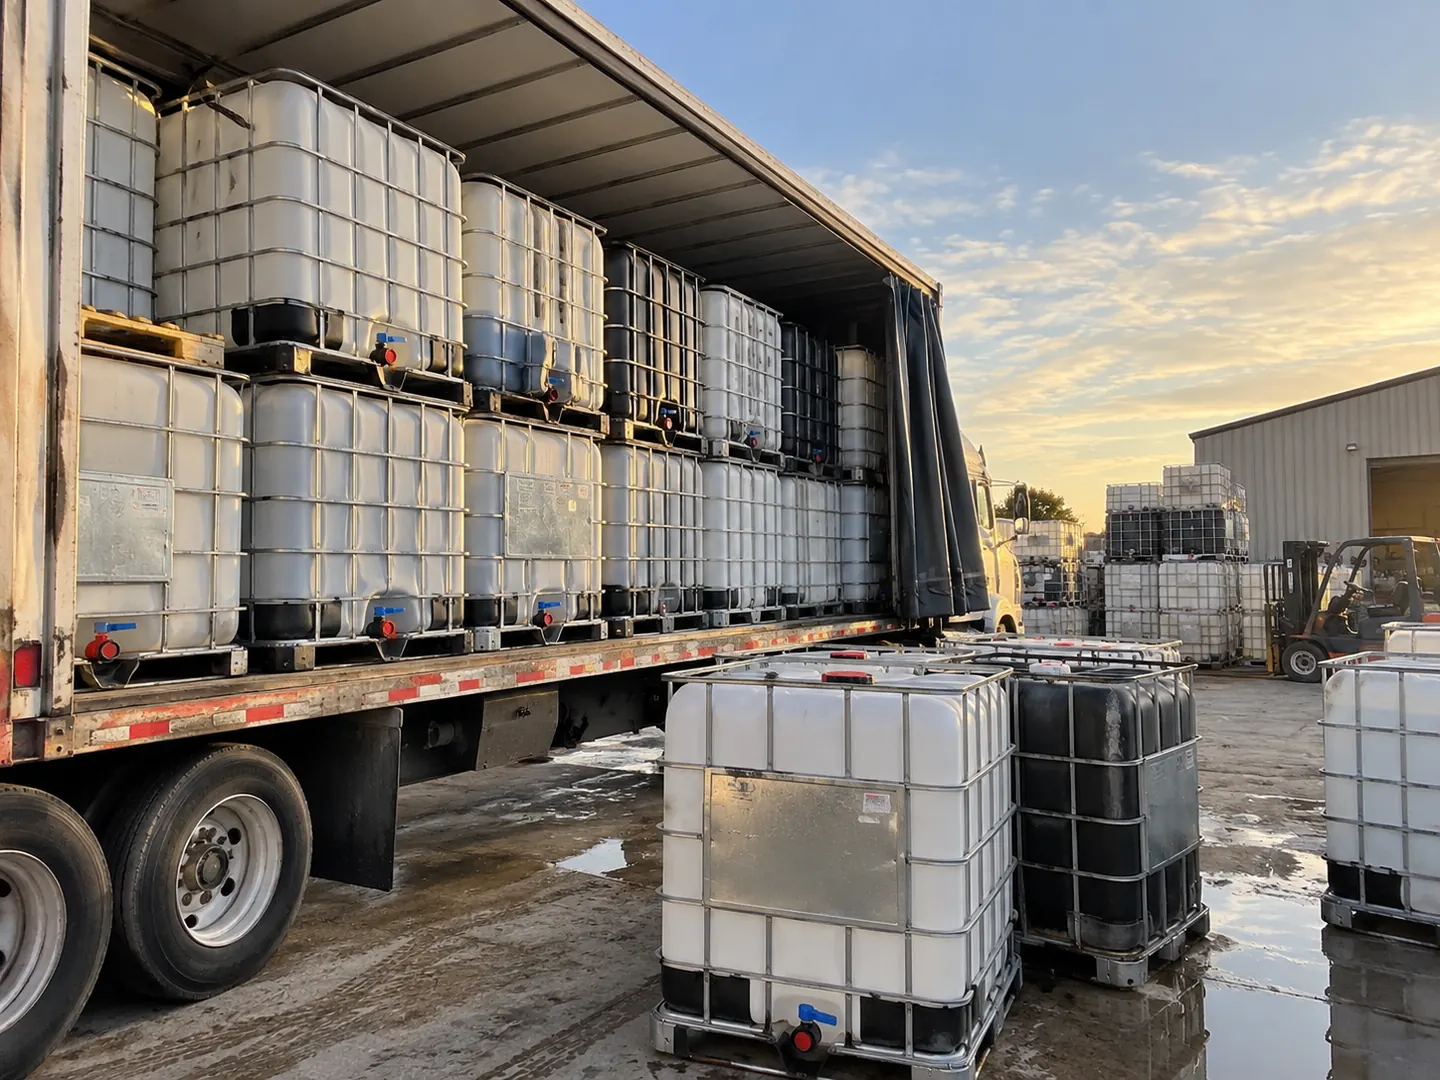
The yard at the hour we start.
How the process actually runs.
Do you wash to a customer's own procedure?
Yes — Route 4. You send the written SOP, we run it and log every parameter it names: temperature, dwell, chemistry and dose, rinse count, verification method, operator, timestamps, all against the cage ID.
This is usually the cleanest way to satisfy an auditor, because the record is in your own format and names your own steps rather than asking somebody to accept ours by analogy.
How do I know the wash record belongs to the container I received?
The cage ID. Every record — intake, wash, leak test, grade, photographs, operator, dates — is keyed to the stamp on the cage you are holding, and the despatch photographs include a shot of that stamp.
Retention is seven years and reissue is a matter of emailing us the cage ID. People do this years later, usually because an auditor has asked a question about a container bought by somebody who has since left.
What does a leak test actually involve?
Pneumatic pressure decay on the complete assembly: pressurise to the design test pressure, hold, and measure the loss. Our pass criterion is under 1 kPa in ten minutes, and the record states method, pressure, hold time and measured decay.
A leak test record with no numbers on it is not a leak test record. That is the single most useful thing to check on any supplier's paperwork, including ours.
Is there anything a wash cannot fix?
Plenty. Crazing, wall loss, a persistent bulge, cracked weld nodes, a failed base weld, heat exposure, an illegible plate — none of those are cleanliness problems and no wash route touches them.
And some cargo we will not try: pesticides, pharmaceutical actives, PFAS formulations, isocyanates, polymerising oils, radiological material, anything fire-affected, and anything nobody will name in writing. Those are refused at the gate, because the downside of being wrong is a drained loop and a contaminated batch.
What is the difference between rinsed and washed?
Route 1 is a rinse: one or two drained charges at ambient to 100 °F, verified visually. It produces Grade B and it is appropriate for a great deal of industrial and agricultural work.
Route 2 is a hot caustic wash: 140 to 160 °F, dosed alkaline detergent, three cascade charges, verified by conductivity and borescope. It produces Grade A washed. The gap between them is not a detail — it is the difference between a container that looks clean and one with a measured number behind it.
How can three rinses use only 11.5 gallons of fresh water?
Because the rinses cascade. The third rinse on one unit becomes the second rinse on the next and the first on the one after, so fresh water enters at the clean end and leaves at the dirty end. Eighty-six percent of bay water is recirculated.
It also means the direction of flow matters more than the volume, which is why the measurement we care about is third-rinse conductivity against the day's measured supply water rather than gallons used.
Can you get a cargo odour out completely?
Usually, and when we cannot the unit drops a grade and we say so rather than hoping you do not notice. Two operators check independently with the cap off at ambient temperature, because that is the check you will make yourself when it arrives.
The commonest cause of a lingering smell in an otherwise clean container is the gasket, not the bottle — the elastomer holds the prior cargo and no amount of rinsing the bottle addresses it. We fit a new gasket on every Grade A and B unit for exactly this reason.
When to retire a container, and what happens to it then.
| Trigger | Severity | Reusable parts | Material route | Take-back value |
|---|---|---|---|---|
| Crazing anywhere on the bottle | Absolute | Cage, base, hardware | HDPE flake, 68% recovery | Partial — cage and base credited |
| Wall loss over 15% of nominal | Absolute | Cage, base, hardware | HDPE flake | Partial |
| Failed leak test after repair | Absolute | Cage, base | HDPE flake | Partial |
| Heat or fire exposure | Absolute, no exceptions | Nothing — all refused | Energy recovery | None |
| Excluded prior cargo | Absolute | Nothing | Licensed disposal | None, and we will say why |
| Persistent bulge over 6 mm | High | Cage, base, hardware | HDPE flake | Partial |
| Cracked weld nodes, three or more | High | Bottle, base | Baled steel, 92% recovery | Partial — bottle credited |
| Base weld failure | High | Bottle, cage | Baled steel | Partial |
| Odour that will not clear | Medium | Cage, base, hardware | HDPE flake | Partial |
| Illegible UN plate | Medium — regulated service only | Everything | Stays in non-regulated service | Full |
| Cosmetic staining | None | Everything | Back to service as Grade C | Full |
| UV chalking, surface only | None for utility use | Everything | Outdoor service as Grade C | Full |
Our standing offer is the same for all of it: when you are finished with a container, we collect and pay, including for units we will only break for material. That is cheaper for us than buying the same steel and resin on the open market, which is the whole argument for a take-back programme existing at all.
How the container in your yard came to be shaped like that.
The modern caged IBC is a surprisingly young object, and almost every feature of it is the fossil of a specific problem.
Drums and nothing between
Liquids moved in 55-gallon drums or in bulk tankers. Anything in between meant handling dozens of drums, which is why the intermediate category was invented at all.
The first rigid composites
A blow-moulded plastic bottle inside a steel frame, sized to a pallet footprint so a forklift could handle it. The idea has not changed since.
The pallet footprint settles
40 × 48 inches in North America, 1,200 × 1,000 mm in Europe. Every trailer count on this site descends from that choice.
UN performance testing
Packagings began to be approved by design type and performance test rather than by prescription, which is where the 31HA1 marking family comes from.
Periodic testing arrives
The 2.5-year leak test and 5-year inspection cycle formalised, creating the date-stamped plate that decides whether a used unit can still carry a regulated cargo.
Reconditioning becomes a trade
Enough units in circulation, and enough value in a steel cage that outlasts three bottles, for washing and rebottling to be businesses rather than favours.
One bay and a used pressure washer
Re:IBCtote starts in a rented bay in metro Detroit, washing totes for local chemical blenders who could not get a straight answer about prior contents.
Grading gets published
We write down the disqualifiers rather than keeping them in an inspector's head, because the arguments about Grade B were taking more time than the washing.
The passport
Every unit gets a record keyed to its cage ID: intake, wash parameters, test results, grade, operator, dates. Seven-year retention, reissuable years later.
38,210 containers
Our largest year: 94.2% diverted, 4.4% residual published rather than rounded away, 4,281 tonnes of CO₂e avoided on factors we publish in full.
Ten questions that tell you what a supplier actually is.
Ask these of us too. A supplier who answers all ten without hesitation is running a real process; one who cannot answer three of them is reselling whatever came in on the last truck.
- What was in this specific unit, and who filled it? Hesitation here is the only red flag that matters.
- What would disqualify this unit from the grade you just sold me? No published disqualifiers means no grading system.
- Can I see photographs of the actual units before I pay, with the cage stamp visible?
- What did the third rinse read, and what did your supply water read that morning?
- Is the gasket new? If not, why am I paying for a clean container with the old cargo's elastomer in it?
- What method, pressure and hold time was the leak test, and what decay did it measure?
- Are the periodic test dates on the plate in date, and will you photograph the plate?
- Are containers and freight quoted as separate lines?
- Will you put in writing what you are not certified for?
- Will you take these back at end of life, and will you pay for them?
Impact questions, answered with the arithmetic.
What happens to the parts you cannot reuse?
HDPE goes to flake at 68% recovery after label and residue loss. Steel is baled and mill-confirmed at 92%. Contaminated fractions go to energy recovery — 535 units' worth in 2025, 1.4% of intake.
The genuine residual is gaskets, labels, adhesive and wash sludge: 4.4% of intake by unit count, 61,428 lb by weight. We publish it rather than rounding it away, and the weight comes from the scale rather than from a unit count.
How do you calculate avoided emissions?
Mass times factor, with every factor published. A reused container avoids the cradle-to-gate impact of the new one it displaced: 42 lb of HDPE at 1.86 kg CO₂e per lb, 55 lb of steel at 0.86, 31 lb of steel pallet at the same, less the 2.3 kg CO₂e of the wash cycle and the freight at 0.40 kg CO₂e per mile.
Where a published range exists we use the end that makes our own numbers look worse — 1.86 against a range up to 2.4 for HDPE, for example. That systematically understates our impact, which is the direction we would rather be wrong in.
Why do you publish a landfill figure?
Because a diversion rate without a residual figure is a marketing number. Ours was 94.2% diverted and 4.4% to landfill in 2025 — gaskets, labels, adhesive and wash sludge, 61,428 lb of it, weighed on the yard scale.
If a supplier quotes you a diversion percentage and cannot immediately tell you what the residual was and what it consisted of, the percentage is not measured. It is estimated, and estimates in this industry drift upward.
Is reuse really better than recycling?
By a wide margin, for this product. Recycling a tote recovers 68% of the HDPE and 92% of the steel and then spends energy turning flake back into a product. Reusing it spends 2.3 kg CO₂e on a wash and keeps 100% of both materials doing the job they were made for.
That is why our disposition table reads 61.4% resold as containers and 18.9% reconditioned, with recycling at 7.2%. Recycling is what we do when reuse has genuinely been exhausted, not as a first resort with a better story attached.
What is the water footprint of a wash?
11.5 gallons of fresh water per container, metered across 2025 and across all four routes, because the rinses cascade and 86% of bay water recirculates.
Against that, making the HDPE bottle it displaced would have used about 4.1 gallons per pound of process water on the low end of the published range — roughly 172 gallons for a 42 lb bottle — plus 1.2 gallons per pound for 86 lb of steel. The wash is not close to being the expensive part.
Can I use your numbers in my own reporting?
Yes, and the methodology document exists for that purpose: every factor, its published range, and which end we chose. Several customers put the disposition record for their own returned units into their annual reporting.
We will also tell you what we do not have: no third-party verified LCA, no certification scheme membership, and a solar installation that covers 31% of yard electricity rather than the number we hoped for, because phase two is sitting in a utility interconnection queue. That list is in the vendor pack too.
What is the single biggest impact in the whole chain?
Making the container in the first place. Everything else — washing, freight, our yard electricity, the fleet — is small against the cradle-to-gate impact of 42 lb of virgin HDPE and 86 lb of virgin steel.
Which means the highest-leverage decision in this entire industry is not which supplier you buy from. It is whether the container you are about to buy needs to be new, and for most cargo the honest answer is no.
From enquiry to units on your dock, in seven steps.
No telephone lines, deliberately. Everything in writing means everything is reviewable later, by you as well as by us.
1 — You tell us the cargo and the end use
Not the grade. The cargo and what you are doing with it. Half the quotes we re-cut are because somebody asked for food-grade to hold site water, and the other half are because somebody asked for Grade B to hold a food product.
2 — We name a grade and say why
With the published disqualifiers attached, so you can see what would drop the unit out of that grade. If a cheaper grade does your job, we say so in the same email — it is a better business than selling you the expensive one once.
3 — Photographs of the actual units
Four per unit plus the cage stamp, tagged to a bay number, before you pay anything. Standard, not a concession, and not a stock image of a different tote.
4 — Containers and freight quoted separately
Two lines, always. A single delivered number hides which of a dozen variables you are paying for, and makes comparing two suppliers impossible.
5 — Load plan against trailer capacity
Twenty on the floor of a 53-foot van, forty double-stacked empty. If your number sits just over a trailer boundary we will tell you which way to move it before you commit.
6 — Despatch with the full record
Prior-contents sheet, wash record with logged parameters, leak test with actual numbers, UN plate photograph, component list, passport ID. One email, with the containers.
7 — Take-back, whenever that is
Months or years later, email the cage IDs. We collect and we pay, including for units that will only be broken for material. The record is still on file for seven years.
Selling us your empties, in six steps.
We buy containers in any condition, including units that will fail every test. Material has value, and a collection that only takes the good ones leaves you with a disposal problem.
1 — Count and name the cargo
How many units, what size, and what was in them — product name and the company that filled them. The cargo decides the price and whether we can take them at all; the condition decides the rest.
2 — Photographs, rough is fine
A phone photograph of the stack and a couple of close-ups of the worst units. We are not grading from photographs, we are checking for the obvious disqualifiers before sending a truck.
3 — Written offer, per unit, by condition band
Not one number for the lot. Good units, utility units and reclaim units are priced separately, so you can see what you are being paid for rather than taking an average on trust.
4 — We schedule onto a lane
If you are on one of our six weekly routes, collection is usually inside the week and costs nothing. Further out we combine with a delivery going your way, which is what backhaul utilisation of 41% is for.
5 — Weighed and counted on arrival
Yard scale, against the manifest. Any discrepancy comes back to you with the scale ticket, in both directions — we have paid out more than was offered more than once.
6 — Payment, and a disposition record
Payment on agreed terms, plus a written record of where your units actually went: resold, rebottled, upcycled, recycled to material, or the residual fraction. Several customers use that record in their own reporting, which is why it exists in that format.
Commercial questions.
Why is one supplier's Grade A cheaper than another's?
Because 'Grade A' is not a standard. It is whatever each supplier means by it, and the only way to compare two of them is to ask what would disqualify a unit from that grade and what records come with it.
A washed unit with one documented food cargo, a logged Route 3 wash, a new gasket and a leak test with numbers on it is a different object from a rinsed unit that looked clean. Both get called Grade A. One of them costs forty percent more and is worth it; the other is a gamble priced like a certainty.
Is it cheaper to buy twenty or to buy five, four times?
Twenty, nearly always, and the reason is freight rather than any volume discount on the containers. Twenty units fill the floor of a 53-foot van, so the freight per unit is at its lowest point on the whole curve.
The cliff is just past it: twenty-two units pays for two trailers to move two containers. If your number is anywhere near a trailer boundary, tell us it is flexible and we will tell you which way to move it.
Do you ever tell people to buy a cheaper grade?
Constantly, and it is the most reliable sales tactic we have. Roughly half the enquiries that ask for food-grade are for site water, dust suppression, ballast or fabrication, where Grade C does the same job for about a third of the price and lasts exactly as long under that treatment.
The money we lose on the first order we get back on the next four, and it means that when we do say you need rebottled, you can believe us.
What does take-back actually pay?
It depends on condition band and on what the cargo was, and we quote it per unit rather than as one number for the lot — good units, utility units and reclaim units priced separately so you can see what you are being paid for.
We pay for units that will fail every test, because a cage is 55 lb of steel at 92% recovery and a bottle is 42 lb of HDPE at 68%. Buying that material from you is cheaper for us than buying it on the open market, which is the whole economic argument for a take-back programme existing.
Why are containers and freight on separate lines?
Because a single delivered number hides which of a dozen variables you are paying for, and makes comparing two quotes impossible. Grade, wash route, hardware, pallet base, plate status, lane, season and quantity all move independently.
It also means that when you come back in six months, we can tell you whether the price moved because resin moved or because diesel moved. If a quote you are comparing does not split them, ask — the answer tells you something either way.
Is there a volume price, and at what point?
The real breaks are at trailer boundaries — twenty, forty, sixty — because that is where freight per unit steps down rather than drifting. Container pricing softens with volume too, but less than people expect, because the cost is dominated by wash bay time and bay time does not get cheaper in bulk.
Scheduled programmes are a different conversation: if you need forty units a month every month, we can hold stock and plan wash capacity around you, and that is worth more to both of us than a one-off discount.
When in the year should I buy?
Late summer for Grade B and C, if your timing is flexible. March to May is the agricultural pull and it puts fifteen to twenty percent on those grades while leaving Grade A almost untouched.
June to August is the softest point of the year on the grades that actually move seasonally. Buying Grade B in August rather than April is the single easiest saving available in this market, and it costs you nothing but storage space.
The twelve-minute check to run when the truck arrives.
Do this before the driver leaves, with the paperwork in your hand. It takes about a minute a unit on a small order and it is the only moment when a problem costs you nothing to raise.
Before anything comes off the trailer
- Count the units and compare against the bill of lading, not against memory.
- Photograph the load in the trailer, from the door, before the first unit moves. This single photograph settles almost every freight-damage dispute.
- Look along the top of the load for crushed cages, which is what a stacked load that shifted looks like.
On each unit, as it lands
- Read the cage stamp and check it against the photographs you were sent. Same unit, or not.
- Cap on and tight? A missing or loose top cap means the unit travelled open.
- Dust cap on the discharge? If it is missing, the valve has been exposed to road spray.
- Open and close the valve through full travel, then wipe it dry and watch it for a minute.
- Look along the lower corners and the sump under a raking light for whitening or cracks.
- Check the diagonals by eye: a cage out of square has been hit.
- Look at the base welds, all four corners, with the unit lifted a couple of inches.
- Read the UN plate and confirm the periodic dates match what you ordered, if your cargo is regulated.
On the paperwork, before you sign
- Prior-contents sheet present, naming product, filler and fill date.
- Grade stated, and the wash record attached if it was Route 2, 3 or 4.
- Leak test record present for every A and B unit, with actual numbers on it.
- Gasket material named on the component list, and matching your cargo.
If something is wrong
Note it on the delivery paperwork before signing and photograph it with the unit's cage stamp in the same frame. Then email us. With a cage ID and a photograph we can pull the intake record, the wash log, the leak test and the despatch photographs within minutes, and the conversation is about facts rather than recollection. Units that are not as described come back on our freight, not yours.
The same containers, different weather.
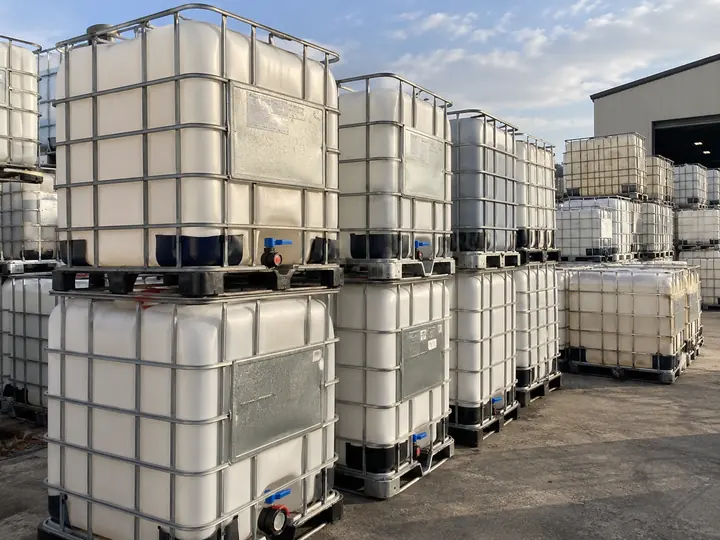
“Half the people who ask us for food-grade are about to put site water in it. Telling them so costs us a third of the invoice and earns the next four orders.”
Send us the cargo, not the grade.
Tell us what is going in the container and what you are doing with it, and we will name the grade, say what would disqualify a unit from it, and tell you if something cheaper does the job. That last part is why people come back.